 ×
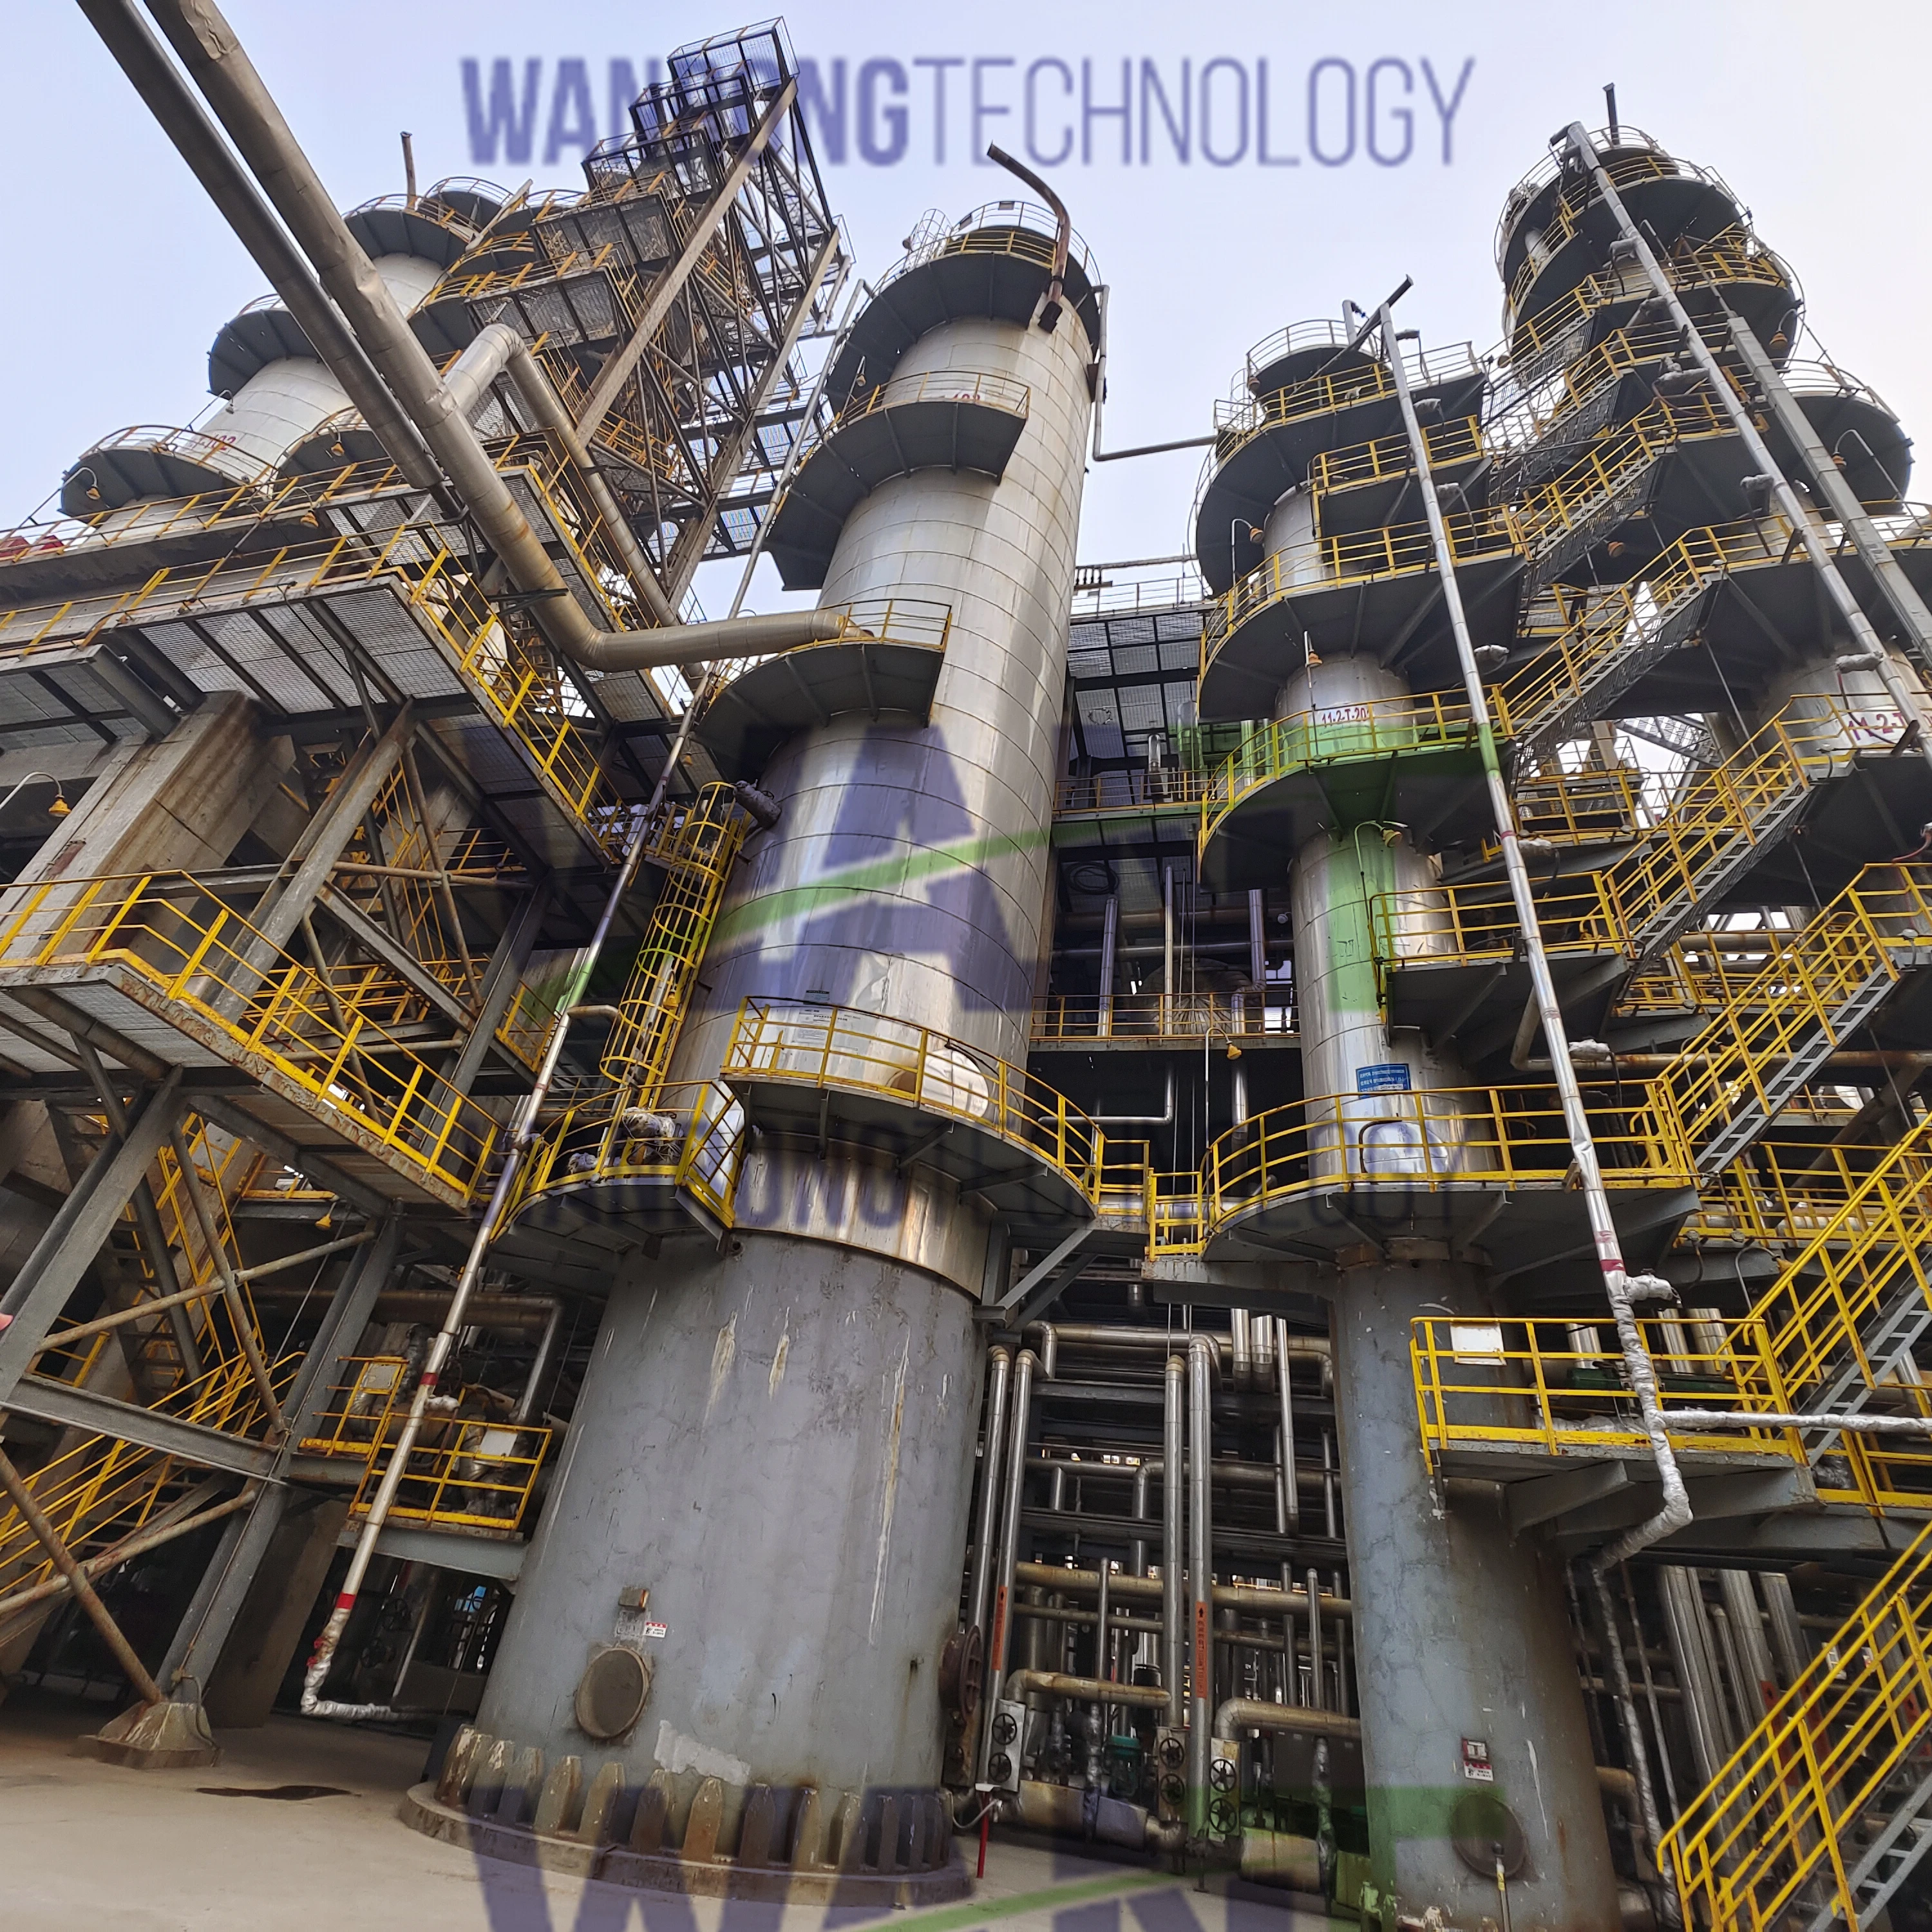
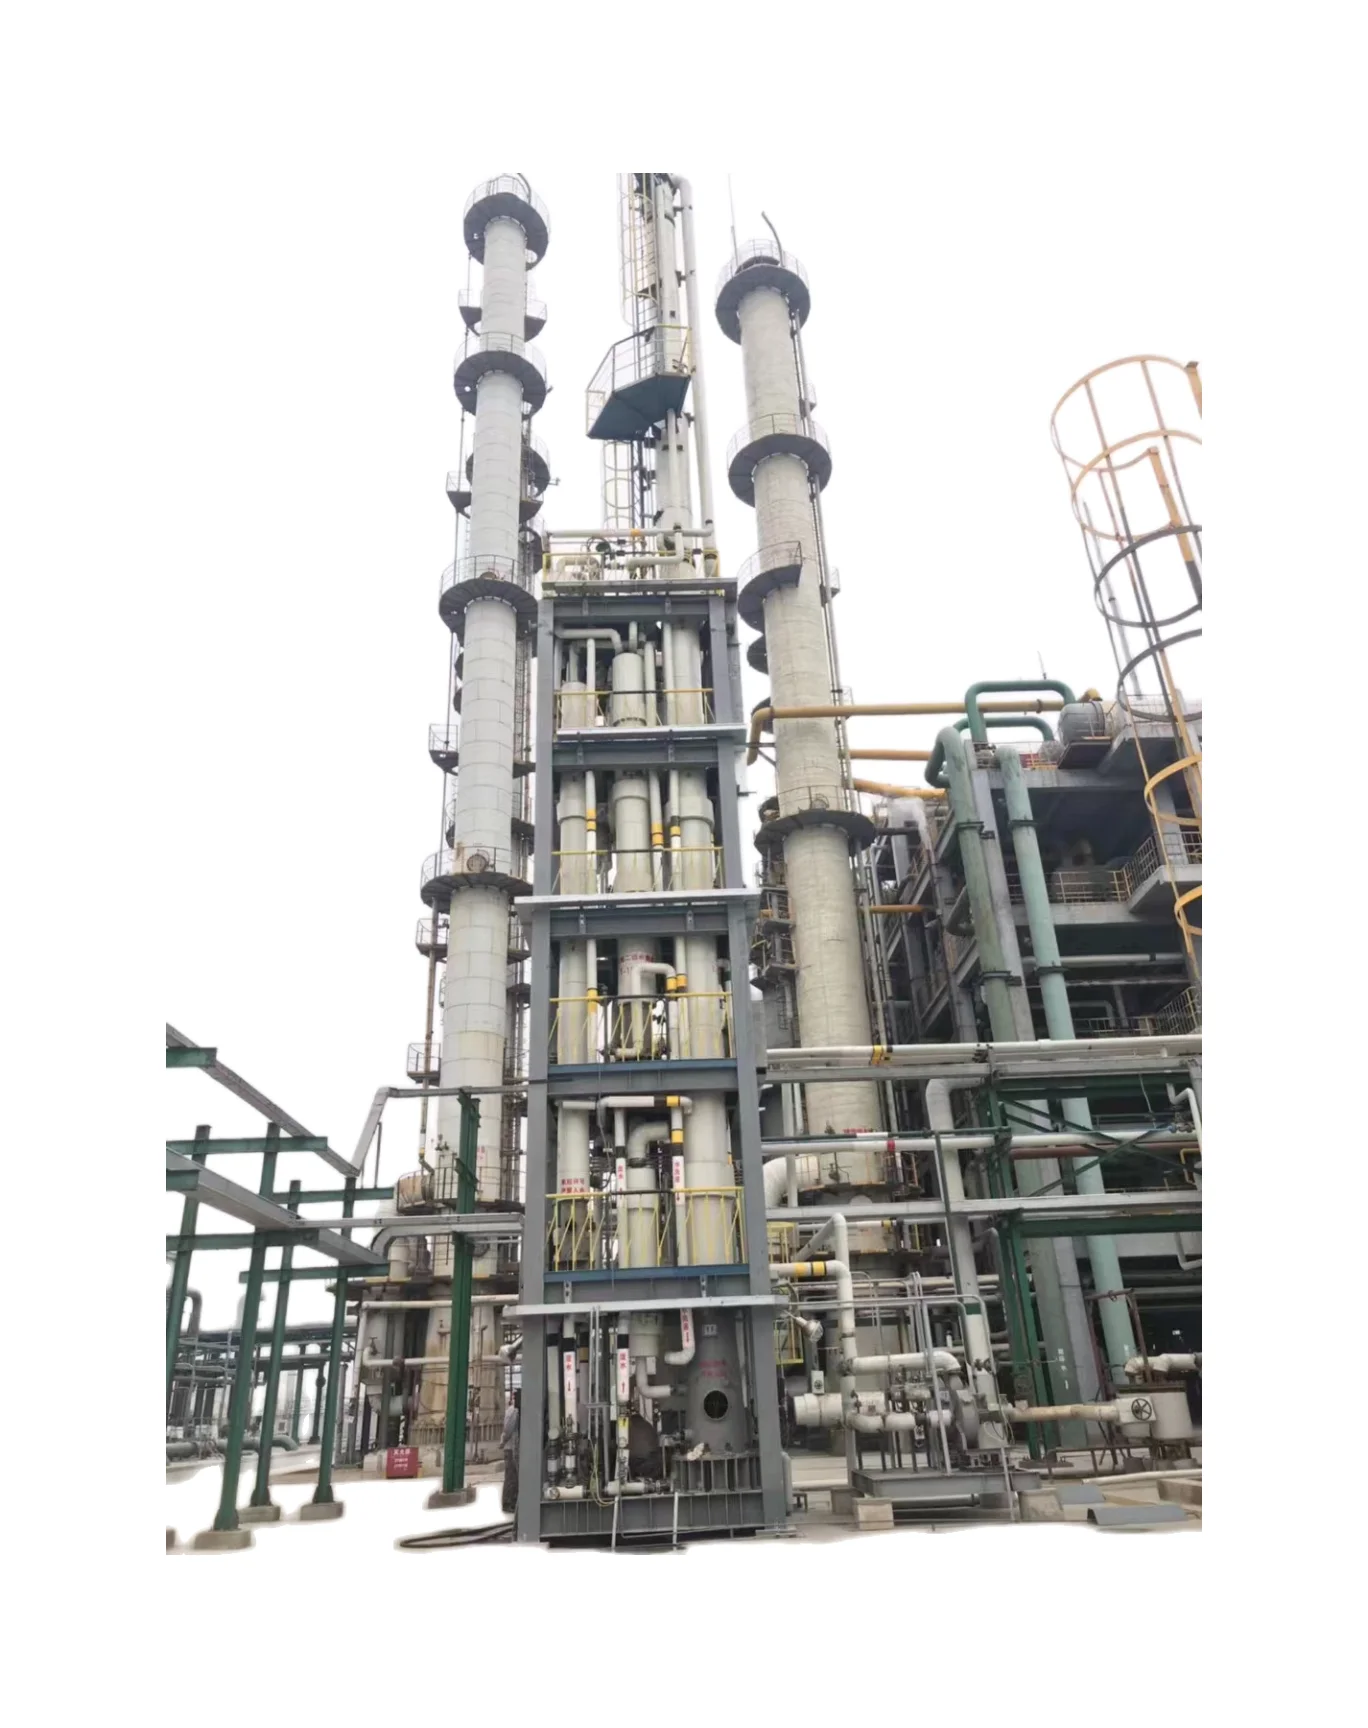
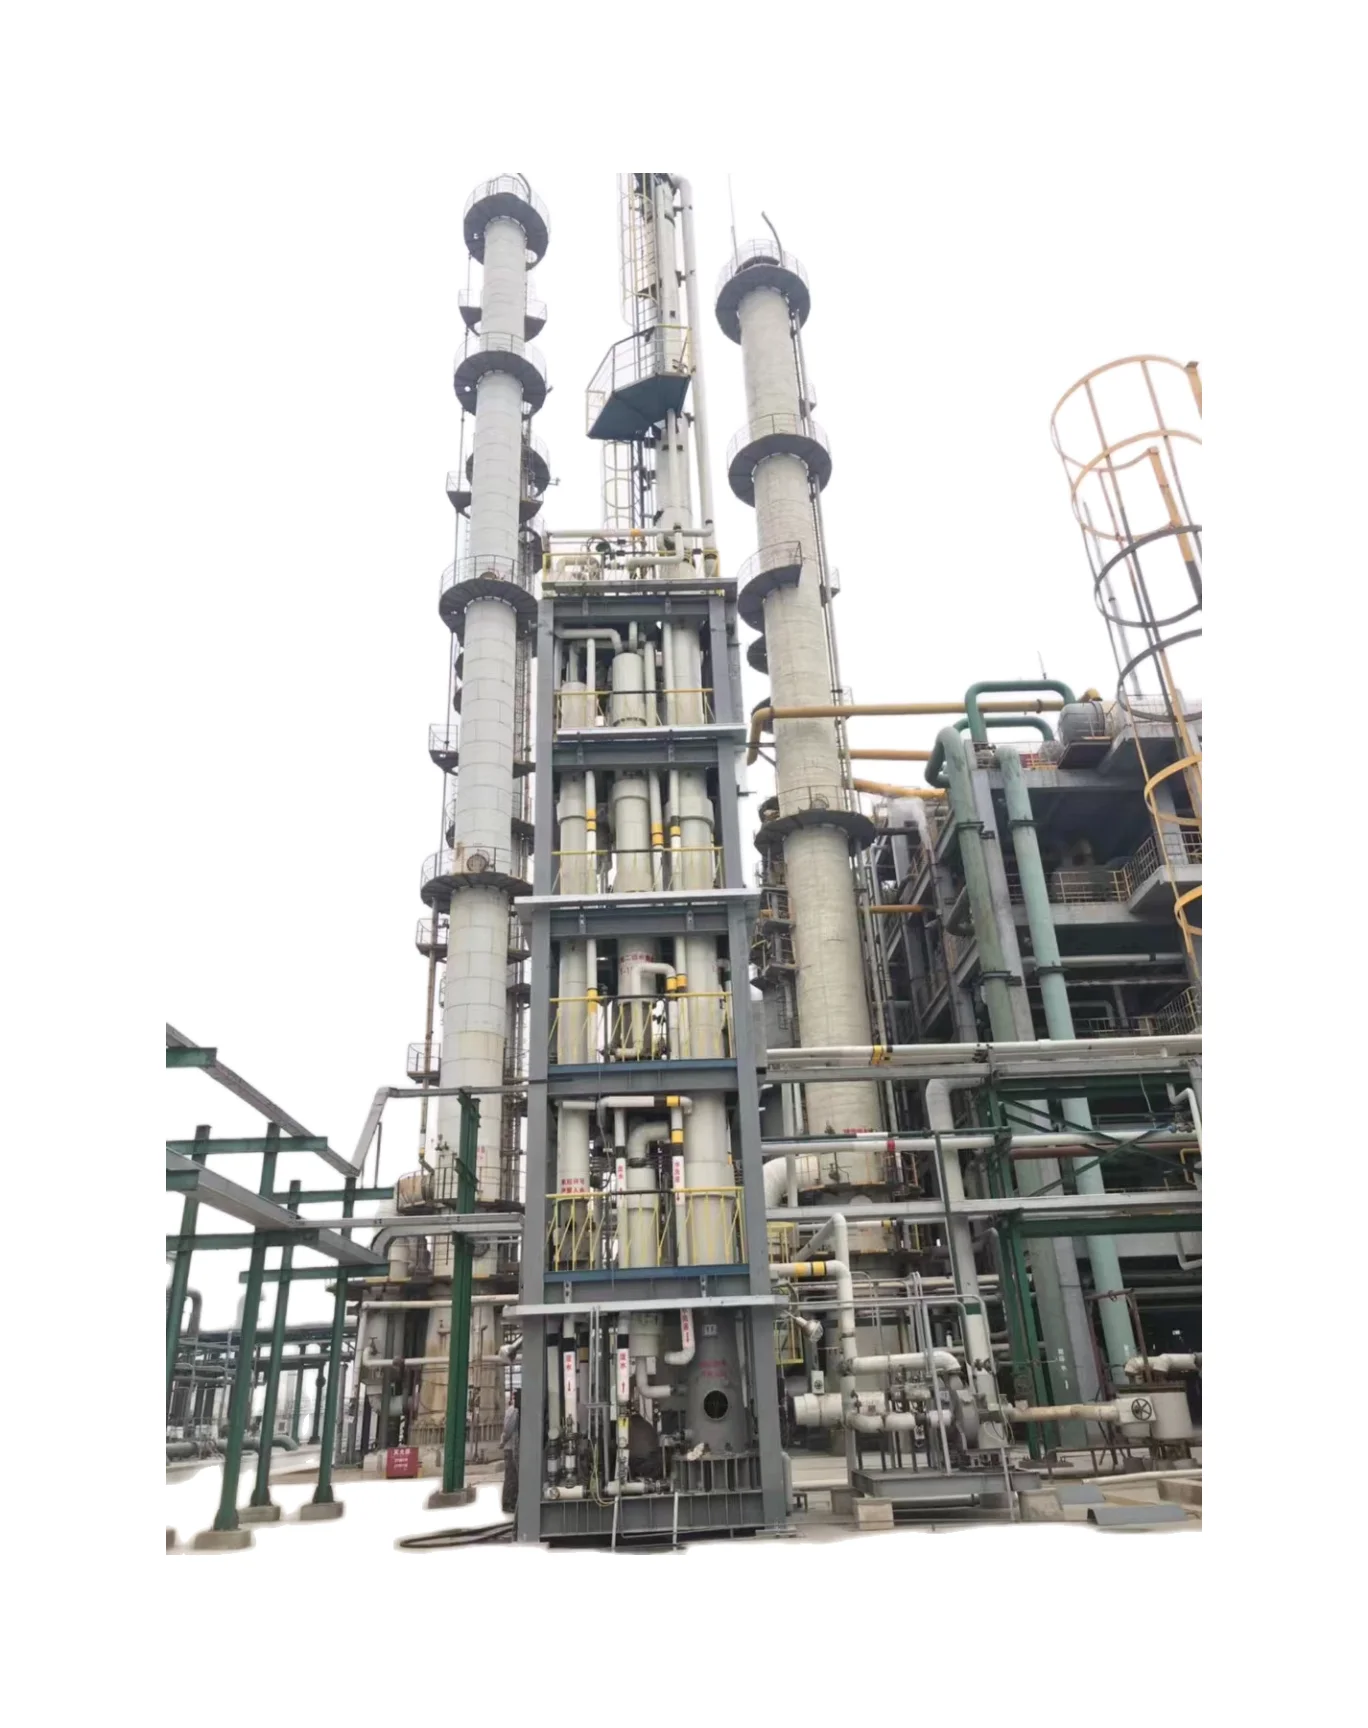
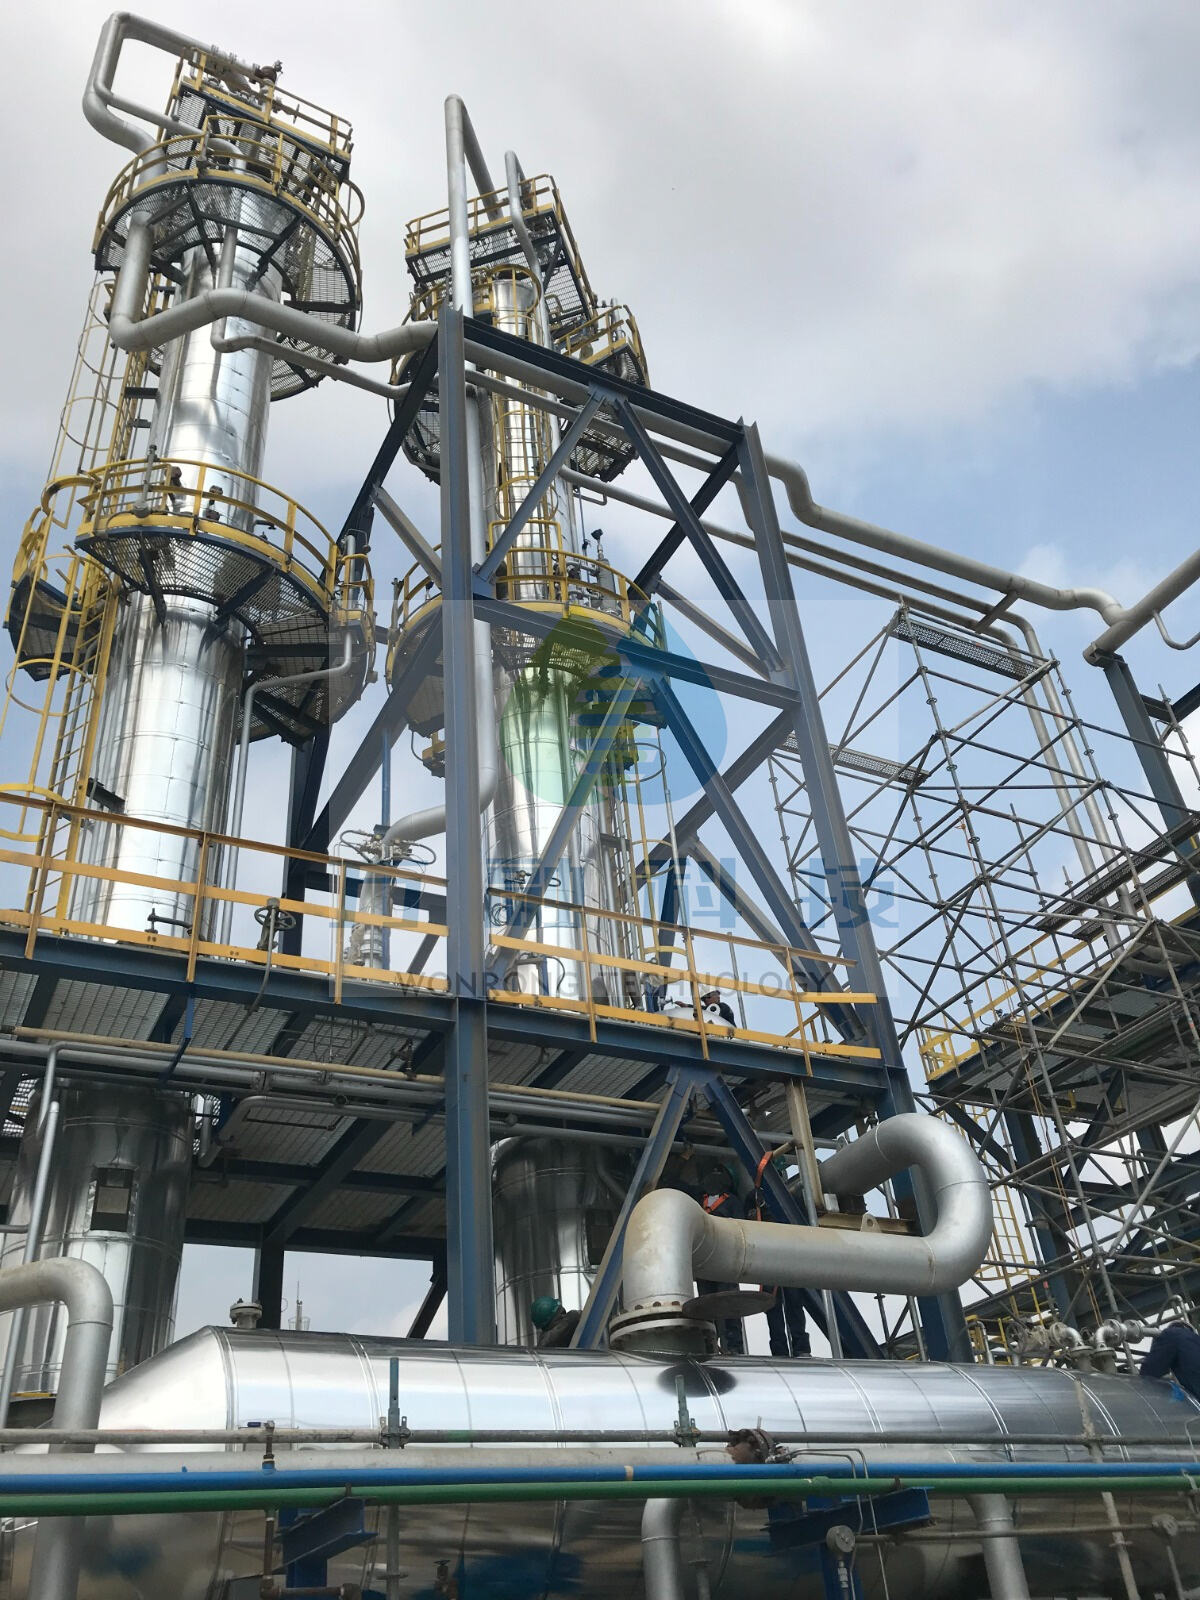
A major benefit of a crude oil refinery tower is that it efficiently separates the different components in crude oil. This makes it possible for refineries to make a variety of petroleum products in response to consumer demand. In addition, the distillation tower can be used to take out impurities from crude oil so that finished products are of good quality. Another benefit is that the distillation tower can run in a continuous fashion to provide refined products activated at a constant. This efficiency ensures low production costs and a constant yield of petroleum products.</p>
In general, a crude oil refinery tower operates by heating crude oil to some very high temperatures so that it becomes vaporized. The vapor is then passed through the trays in a column, the temperature rising as the rock strata are ascended. The vapor rises and becomes cooler before turning to liquid form. It cools the various fractions of crude oil are cooled to various condensation temperatures at which they can be gathered up separately. Other substances such as gasoline form components at lower temperatures, while diesel is formed at greater temperatures. This distillation process is what separates the crude oil into its distinct components, each of which can be refined into various petroleum products. A crude oil refinery unit essentially serves as a key participant in the oils that we use in our daily lifestyle, which nowadays can fundamentally refine various fuels and products.</p>
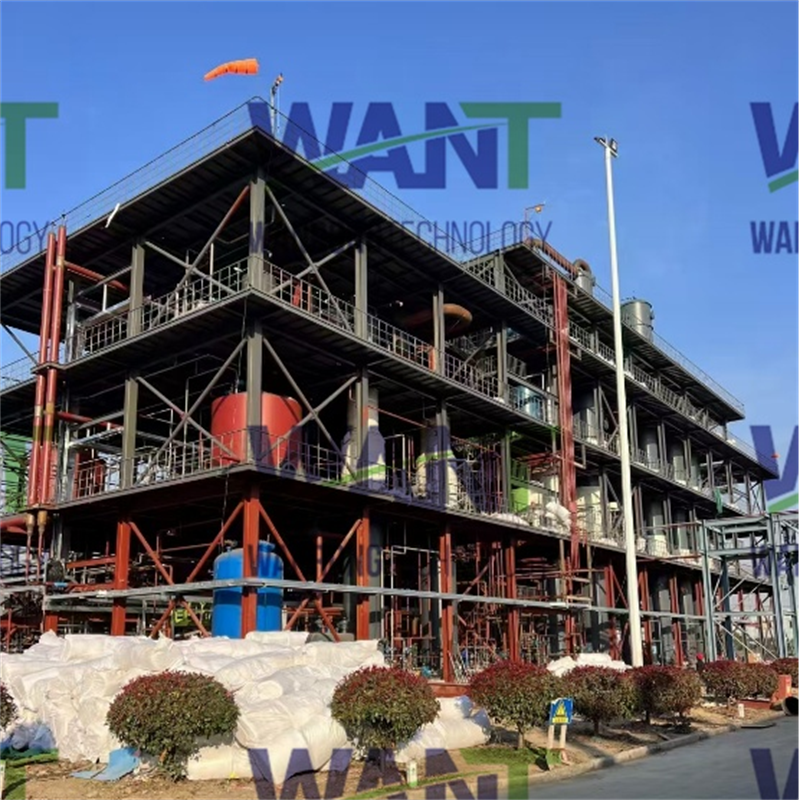
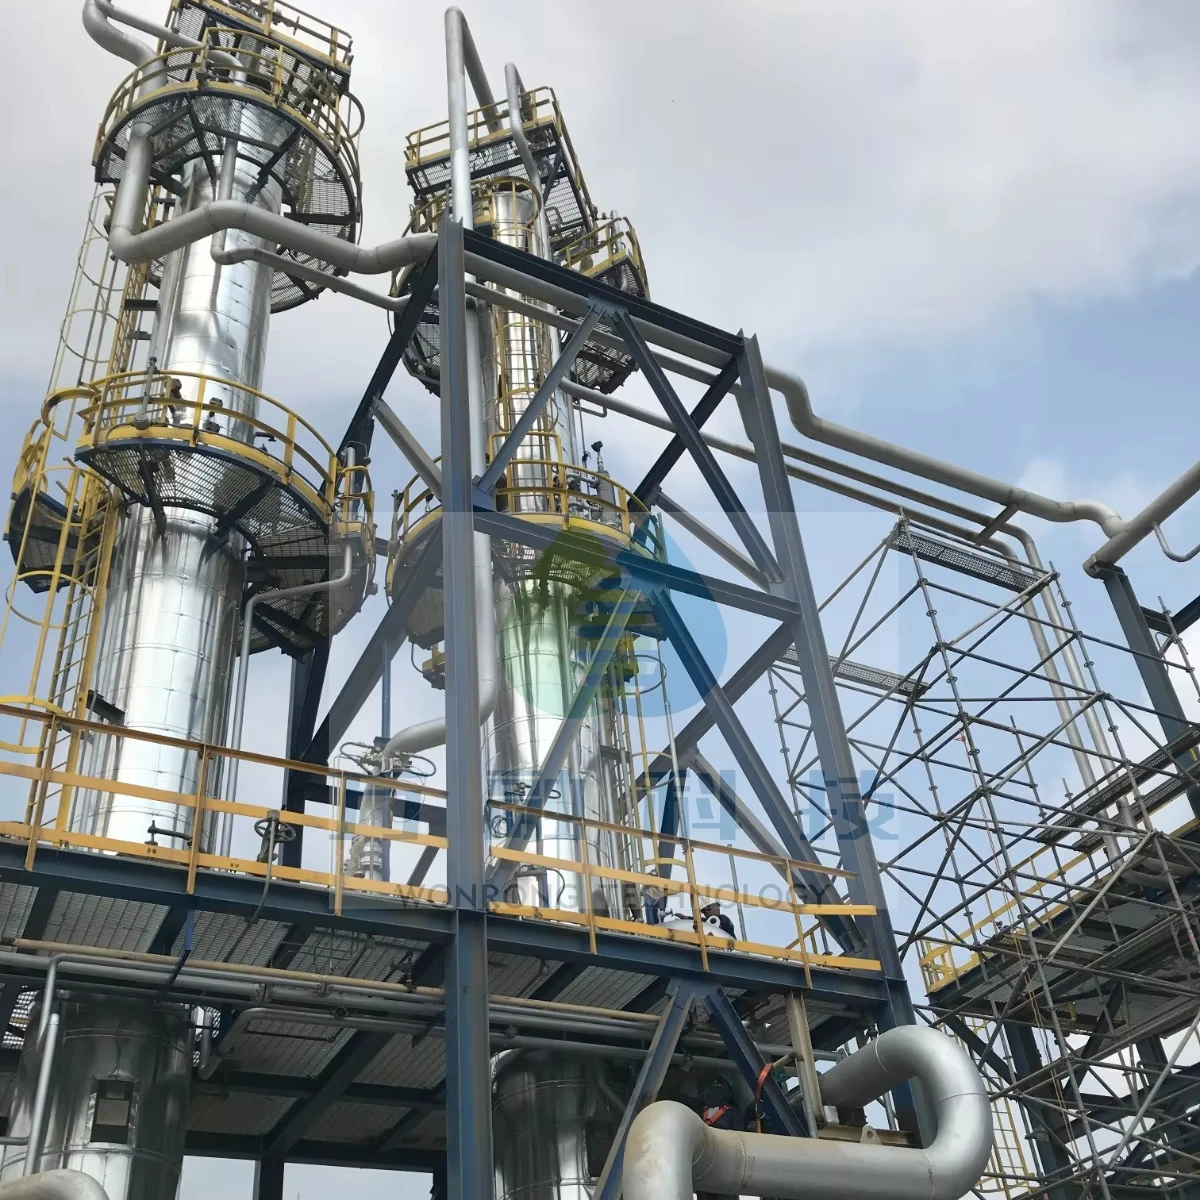
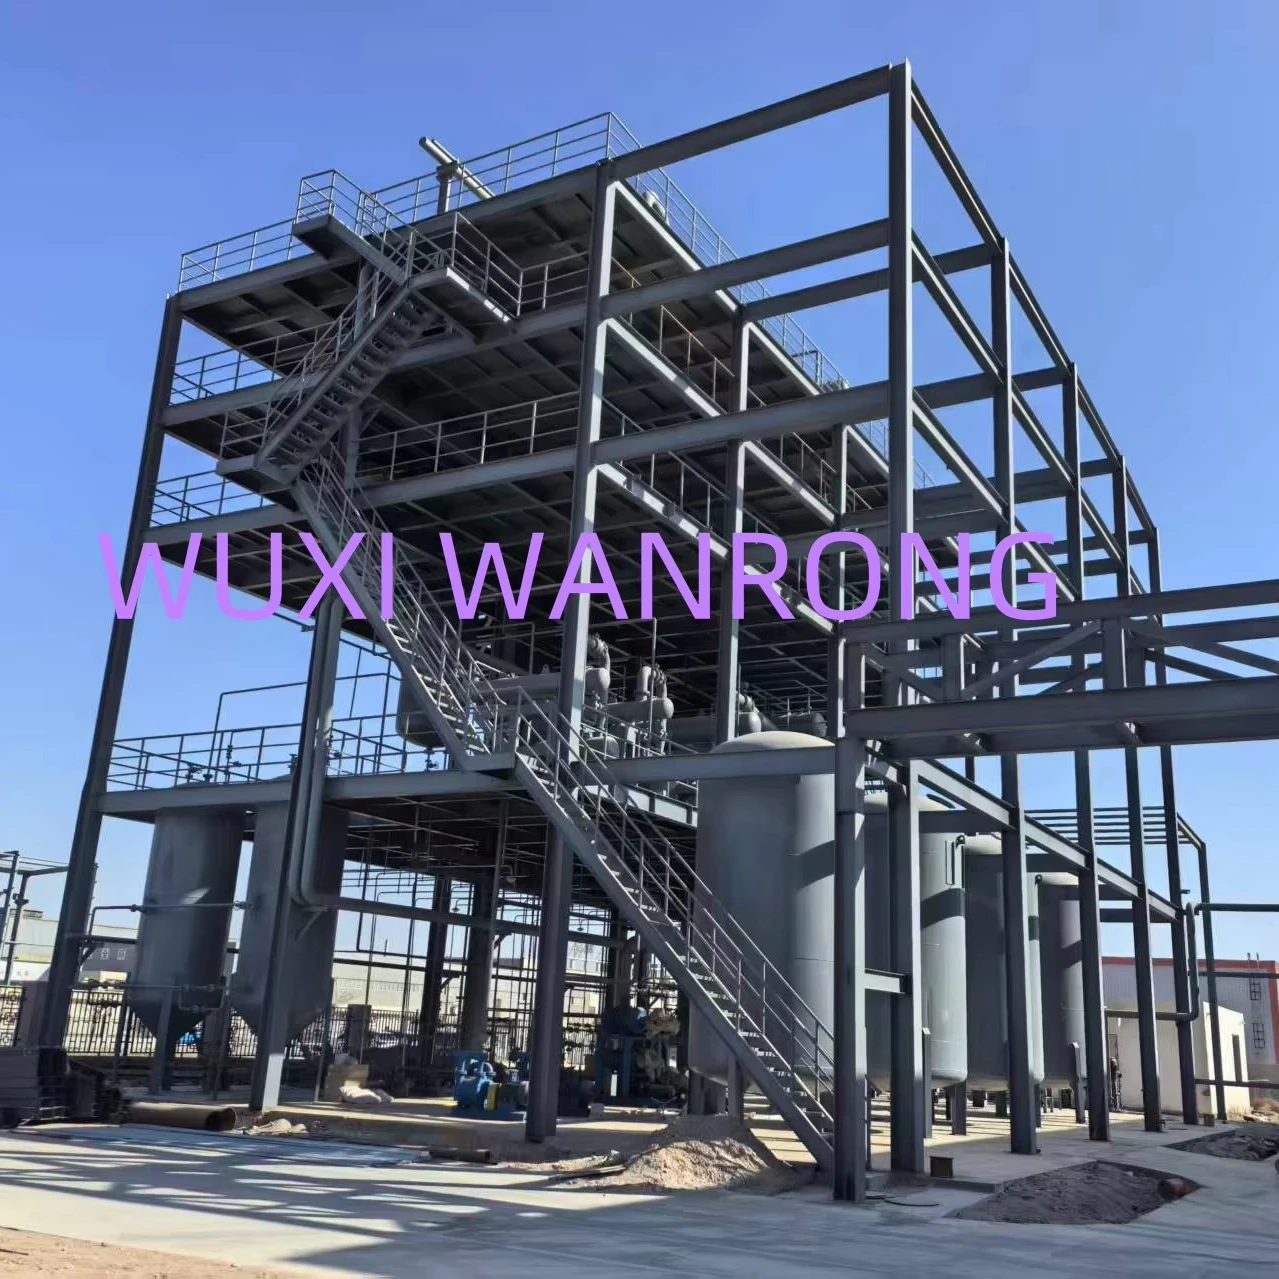
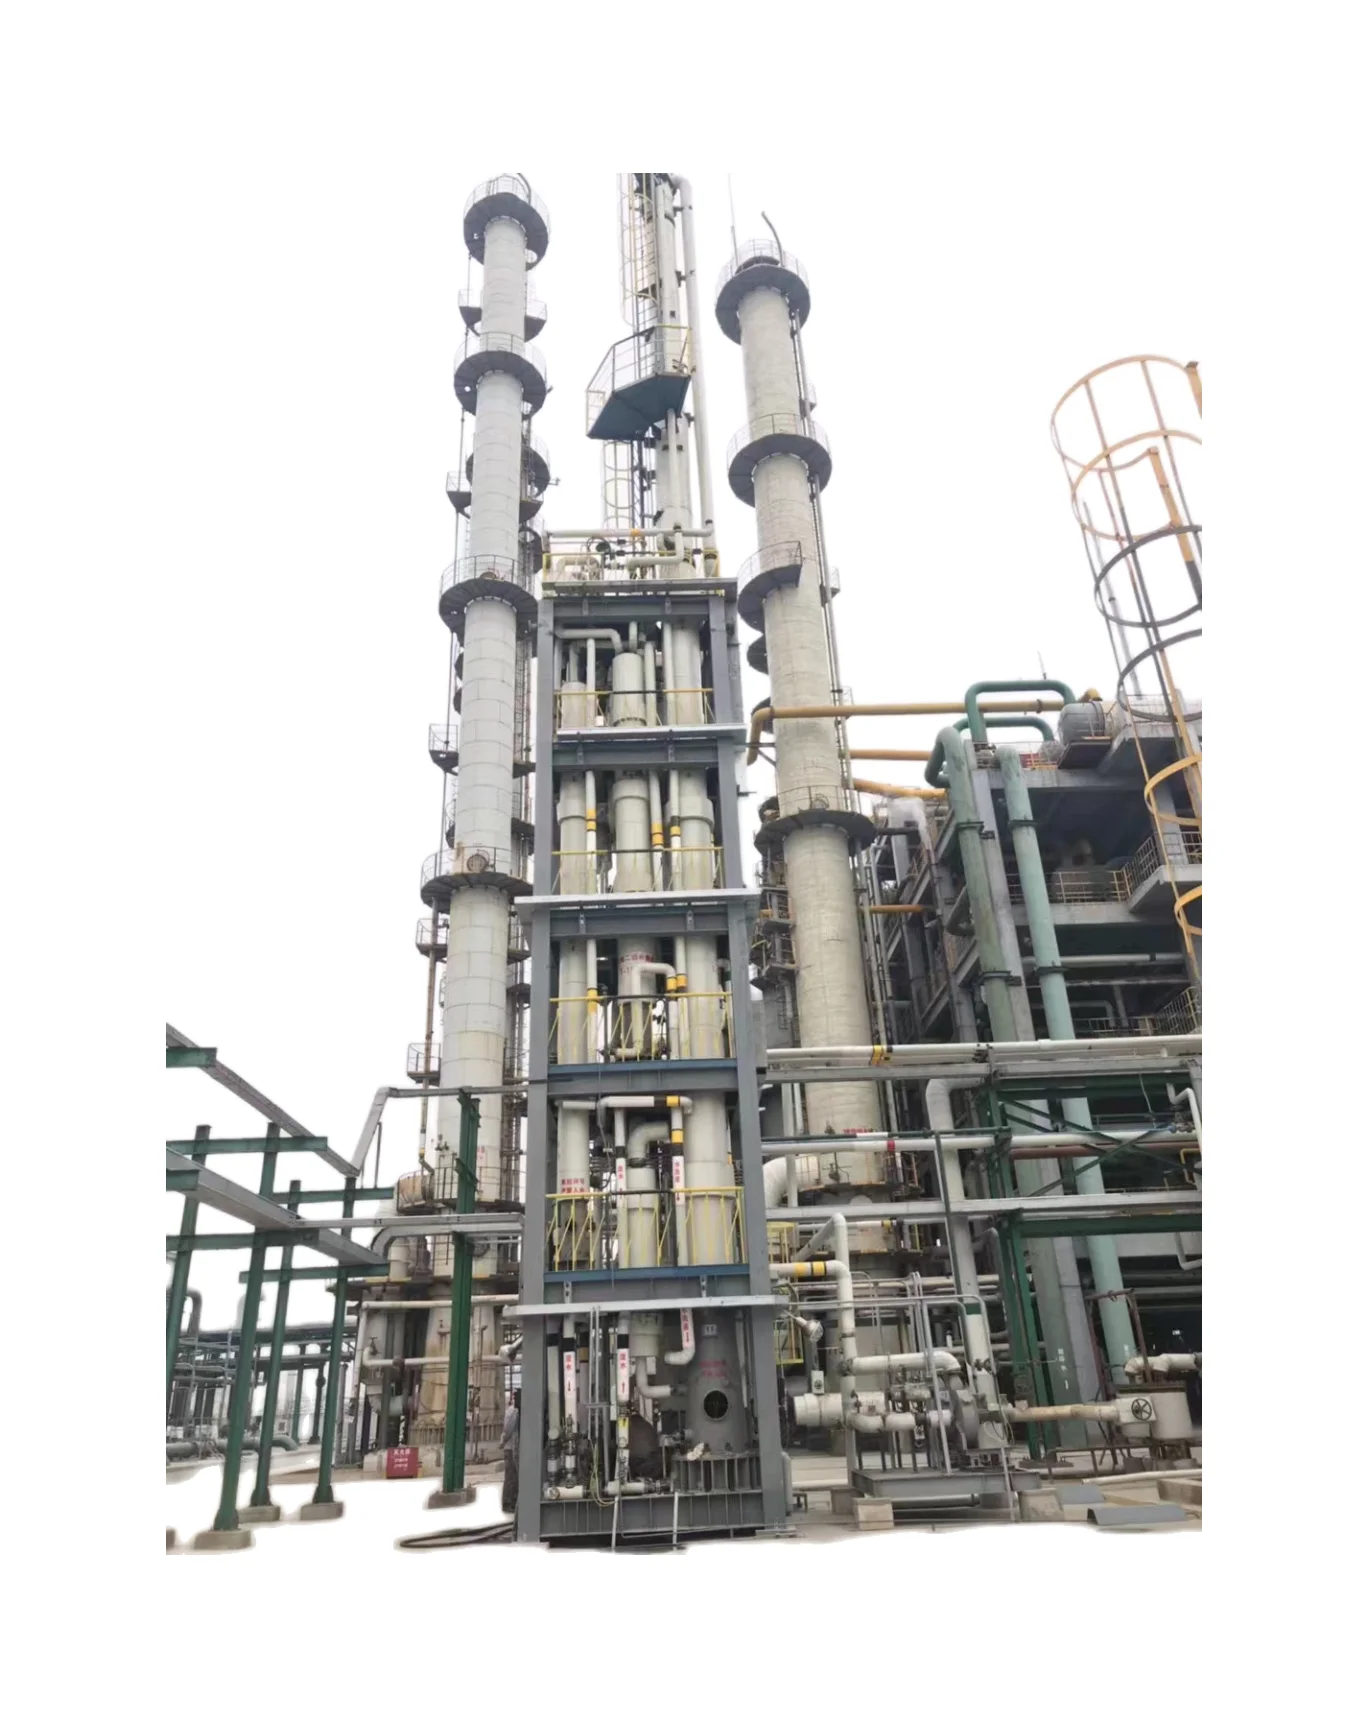
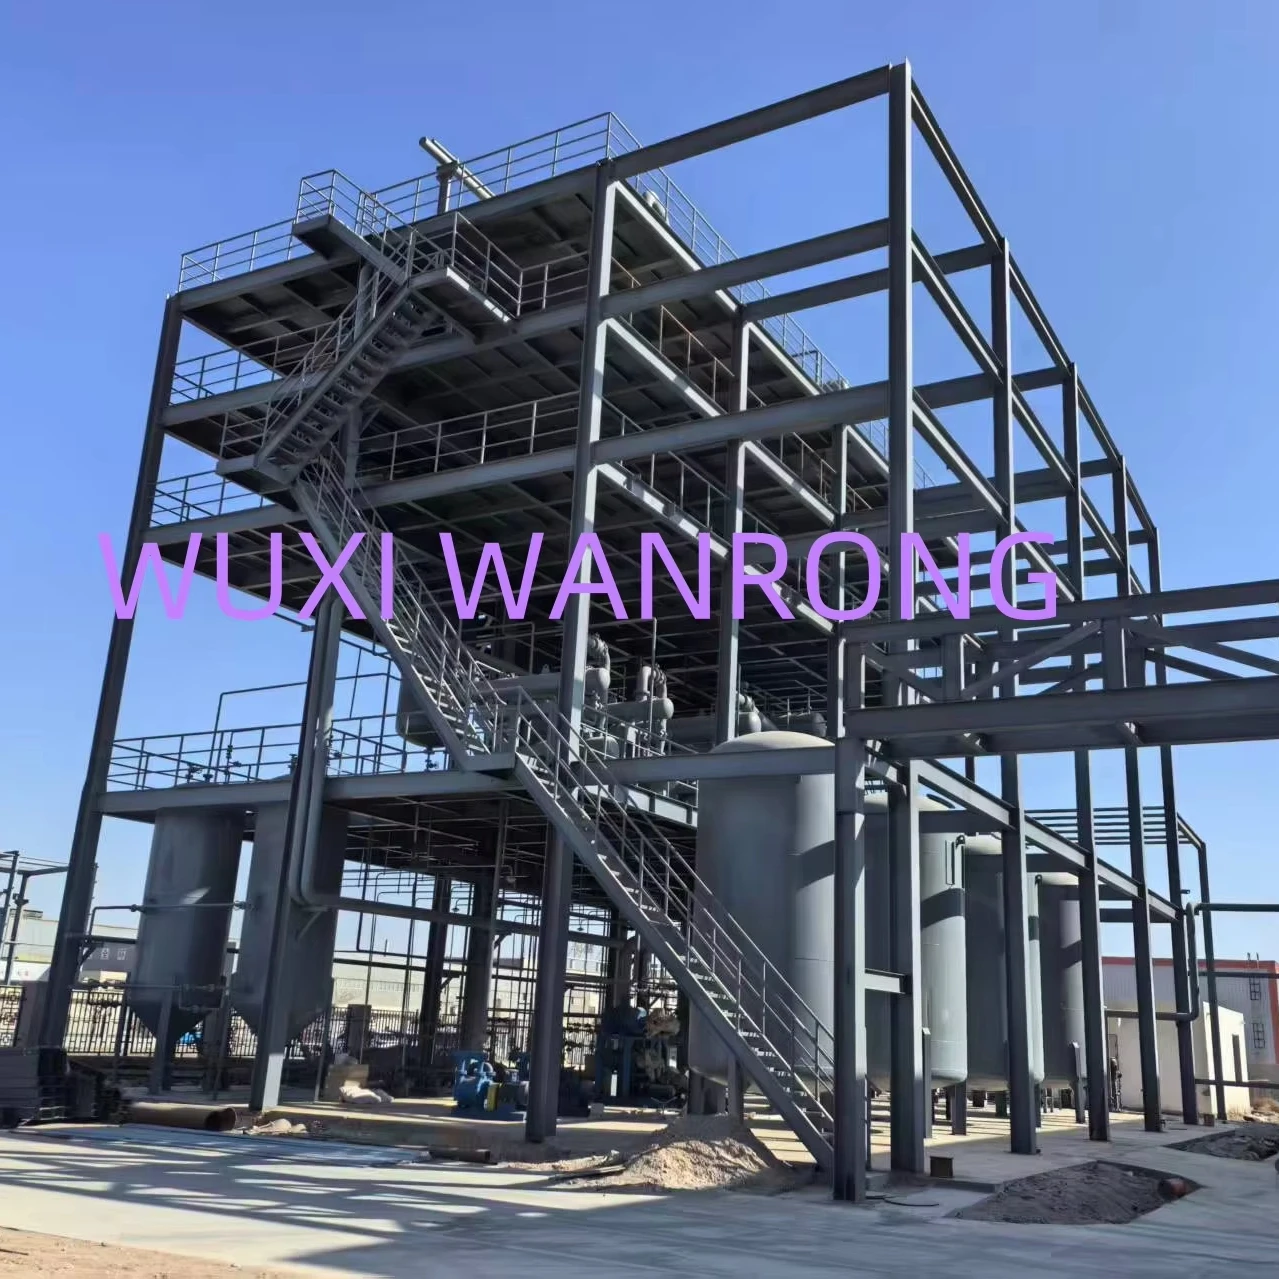
If you are seeking competitive wholesale prices on crude oil distillation columns, the quality and performance of such equipment is paramount. We provide distillation towers to divide crude oil into its components, including gasoline, diesel, and aviation fuel. They are constructed with quality materials for strength and durability you can hear and feel.</p>
WANRONG's crude oil refinery distillation towers are also available in a range of sizes and capacity to meet different production requirements. At the small refinery or a complex large plant, we can find the distillation tower which they need. In addition, custom design of the tower in order to meet individual operating requirements is furnished by WAN RONG, thus to guarantee the maximum performance and economic operation.</p>
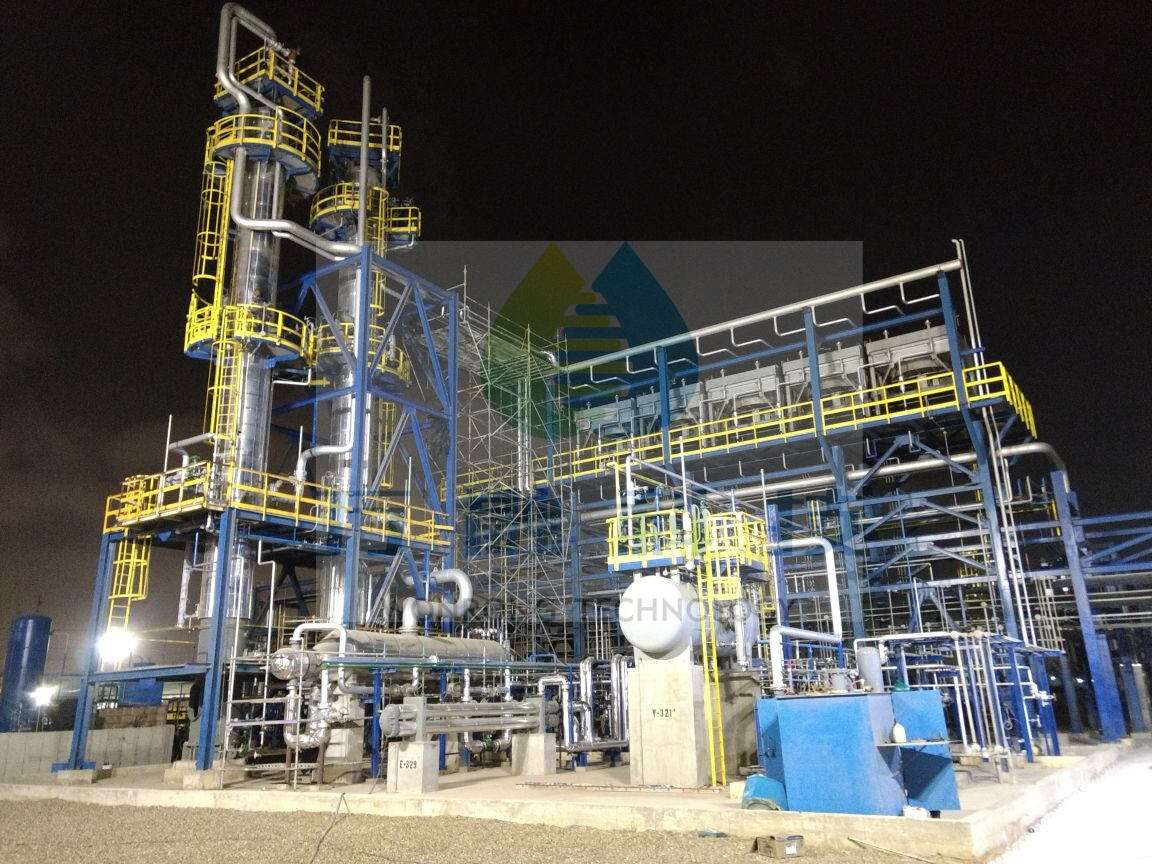
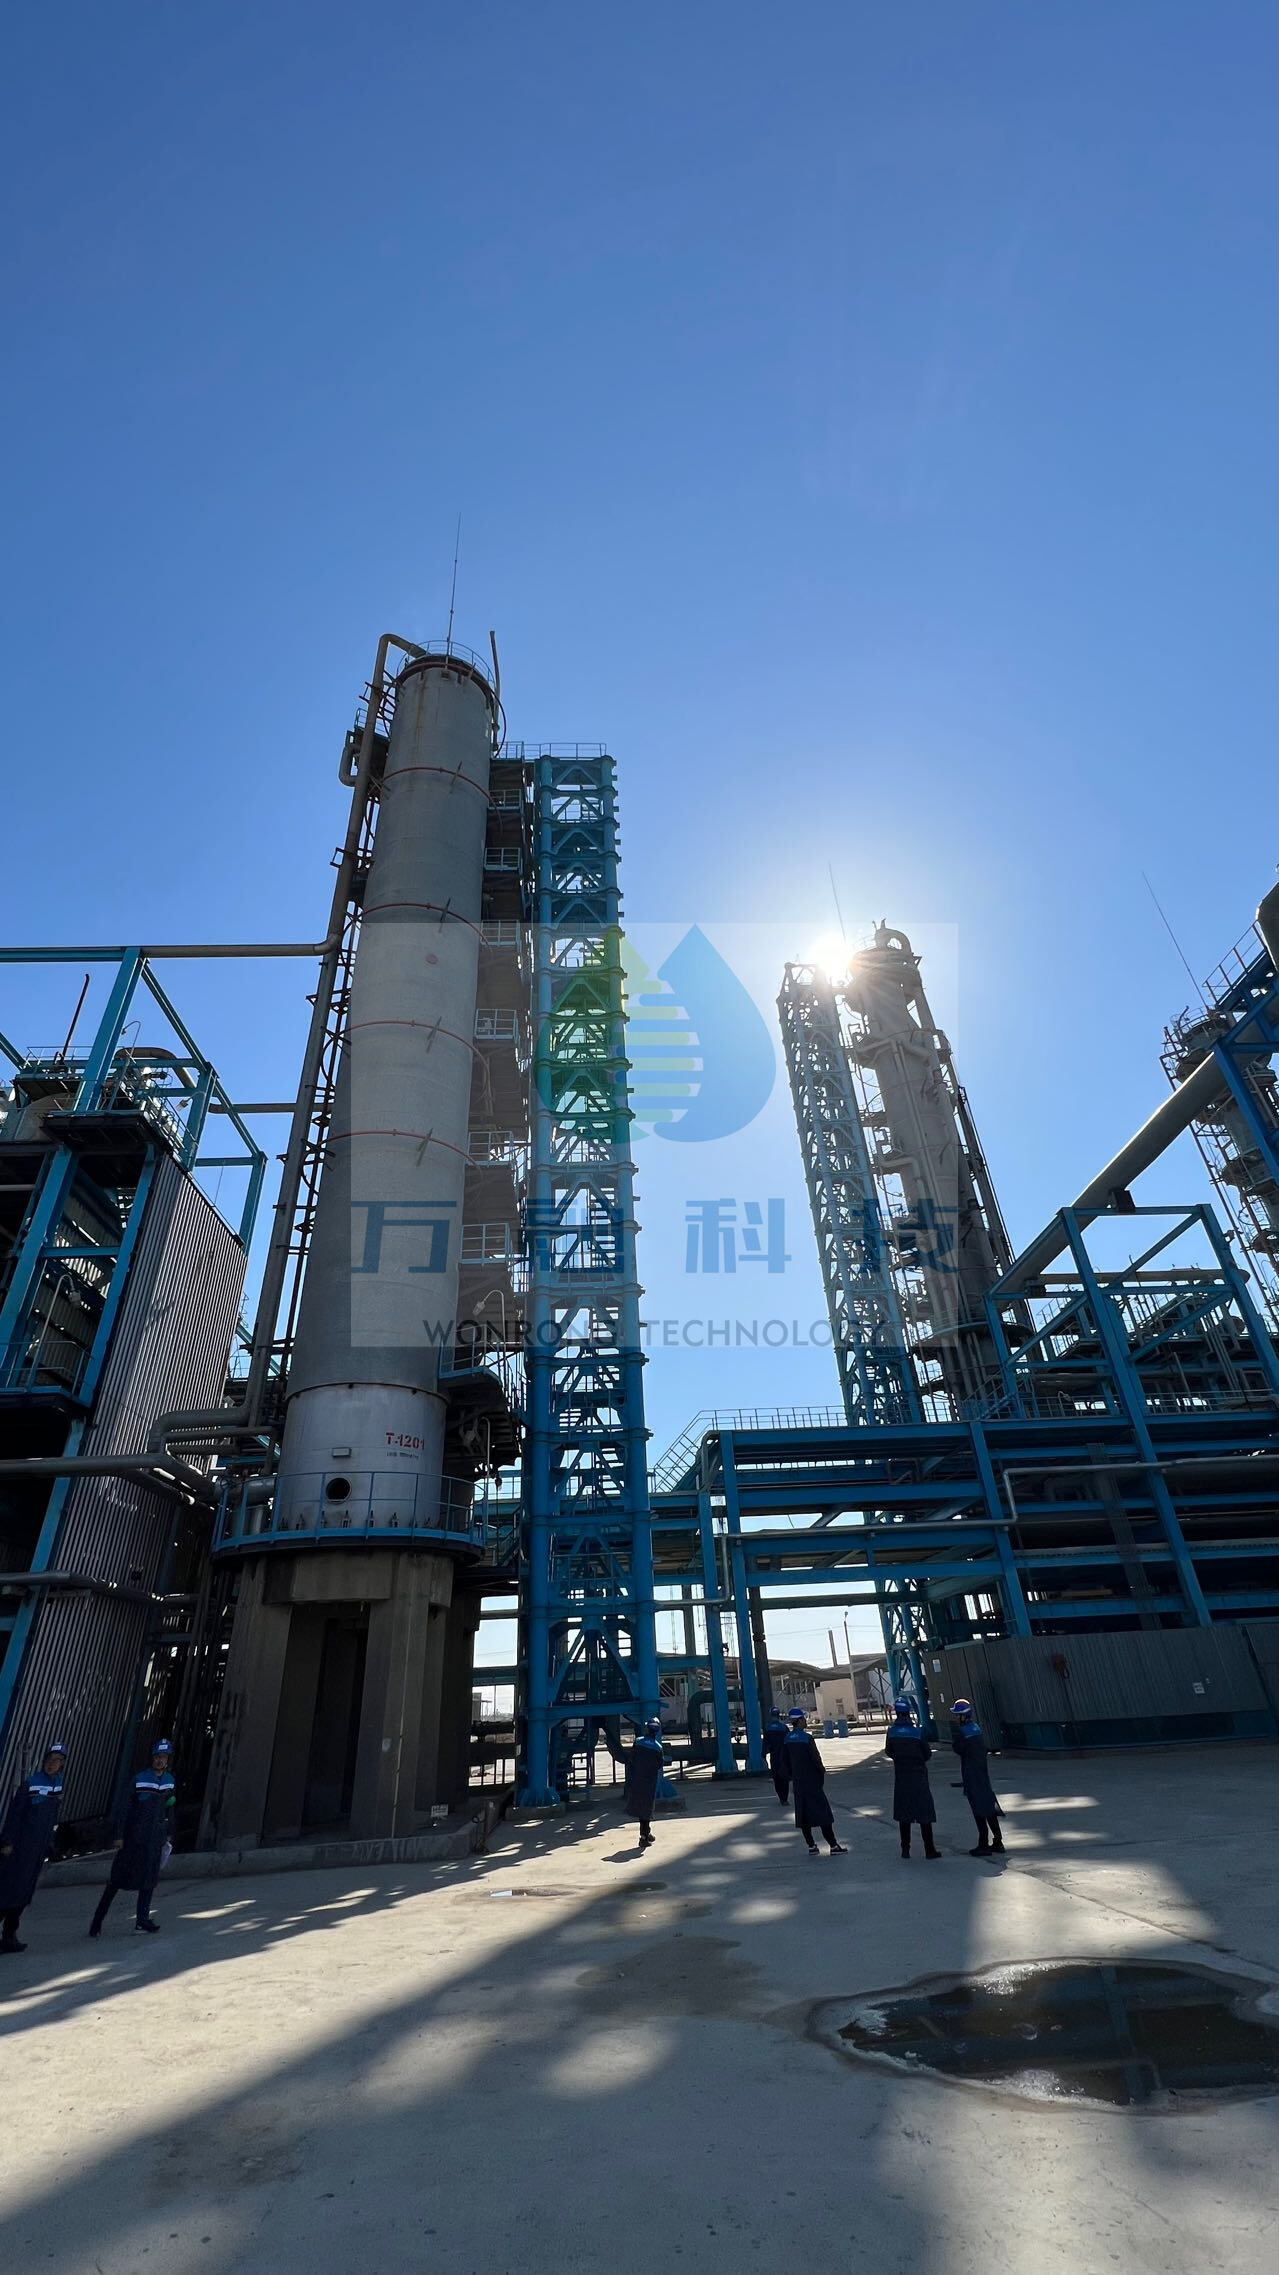
Our close cooperation with top research institutes like Sinopec Shanghai and Nanjing Chemical Research Institute ensures continuous technological advancement, validated through rigorous simulation using Aspen and Plant 3D, keeping us at the forefront of hydrocarbon processing and environmental solutions.
We provide customized, turnkey EPC/EPCC solutions—from design and simulation to fabrication, testing, and commissioning—supported by a worldwide service network to ensure efficient, reliable project execution for clients across Asia, Africa, the Middle East, and beyond.
Adhering to stringent international standards (ASME, PED, ISO, API) and implementing a full-cycle QC system with 217+ checkpoints, we ensure every piece of equipment meets exacting specifications for performance, safety, and durability in global markets.
We offer advanced, integrated technologies across the hydrocarbon value chain—from waste oil regeneration, crude oil hydrogenation, and high-purity gas separation to API-certified base oil production—enabling clients to achieve both profitability and environmental compliance.
Copyright © Wuxi Wanrong Environmental Protection Technology Co.,Ltd. All Rights Reserved

 EN