 ×
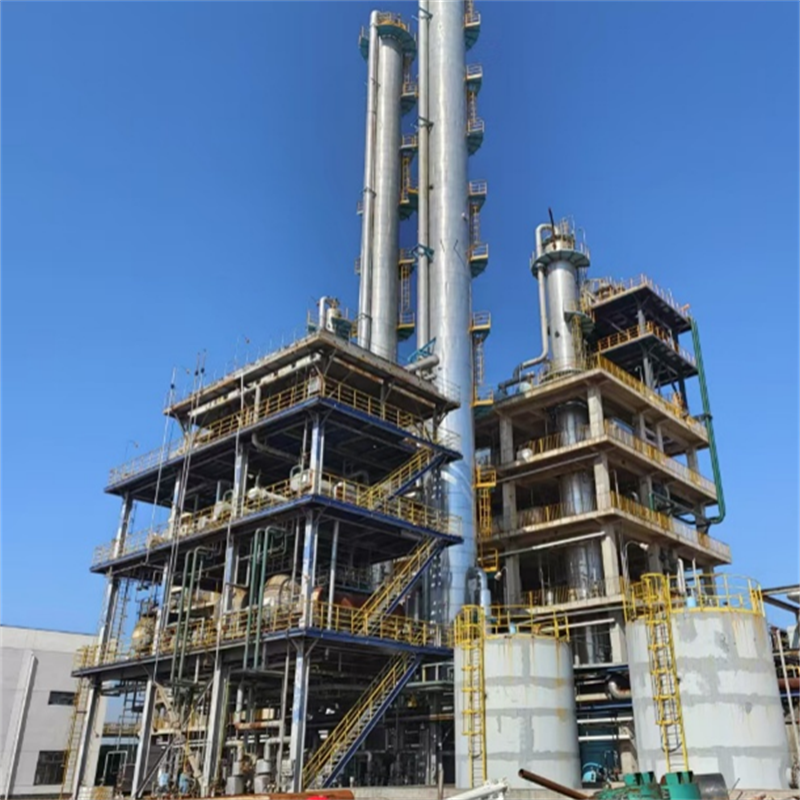
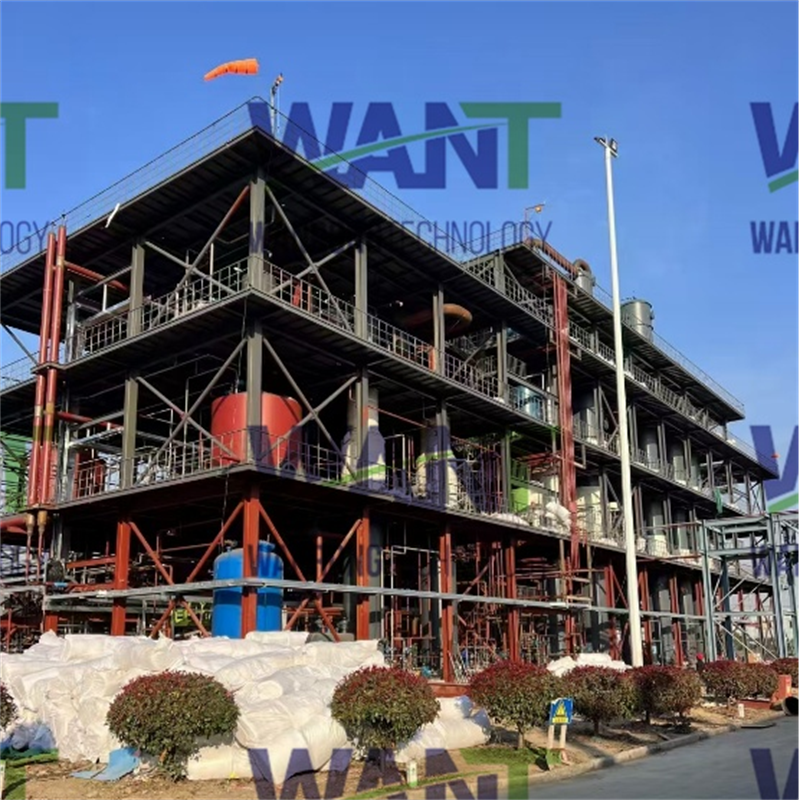
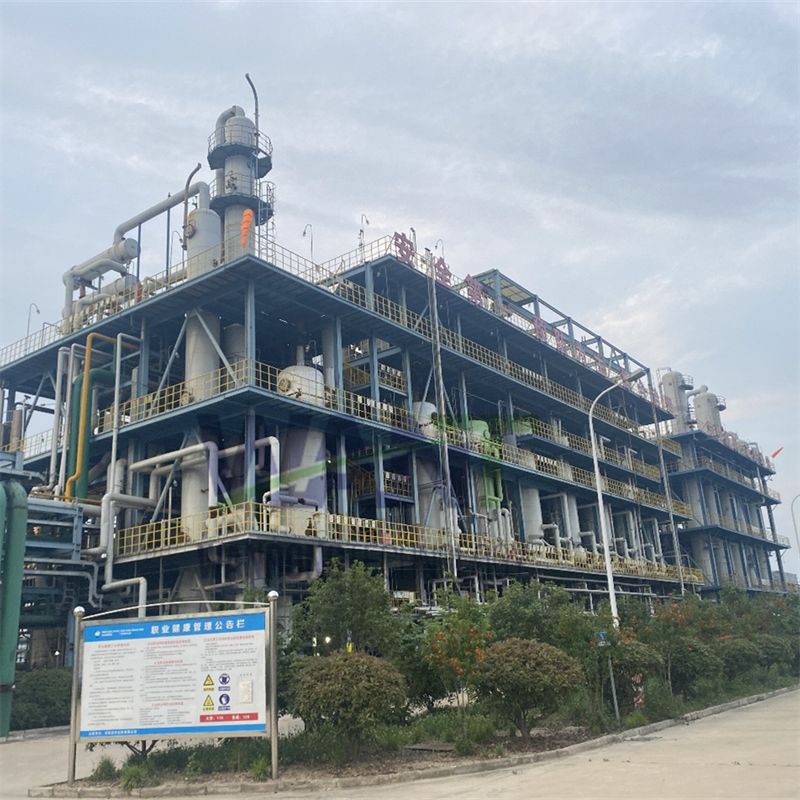
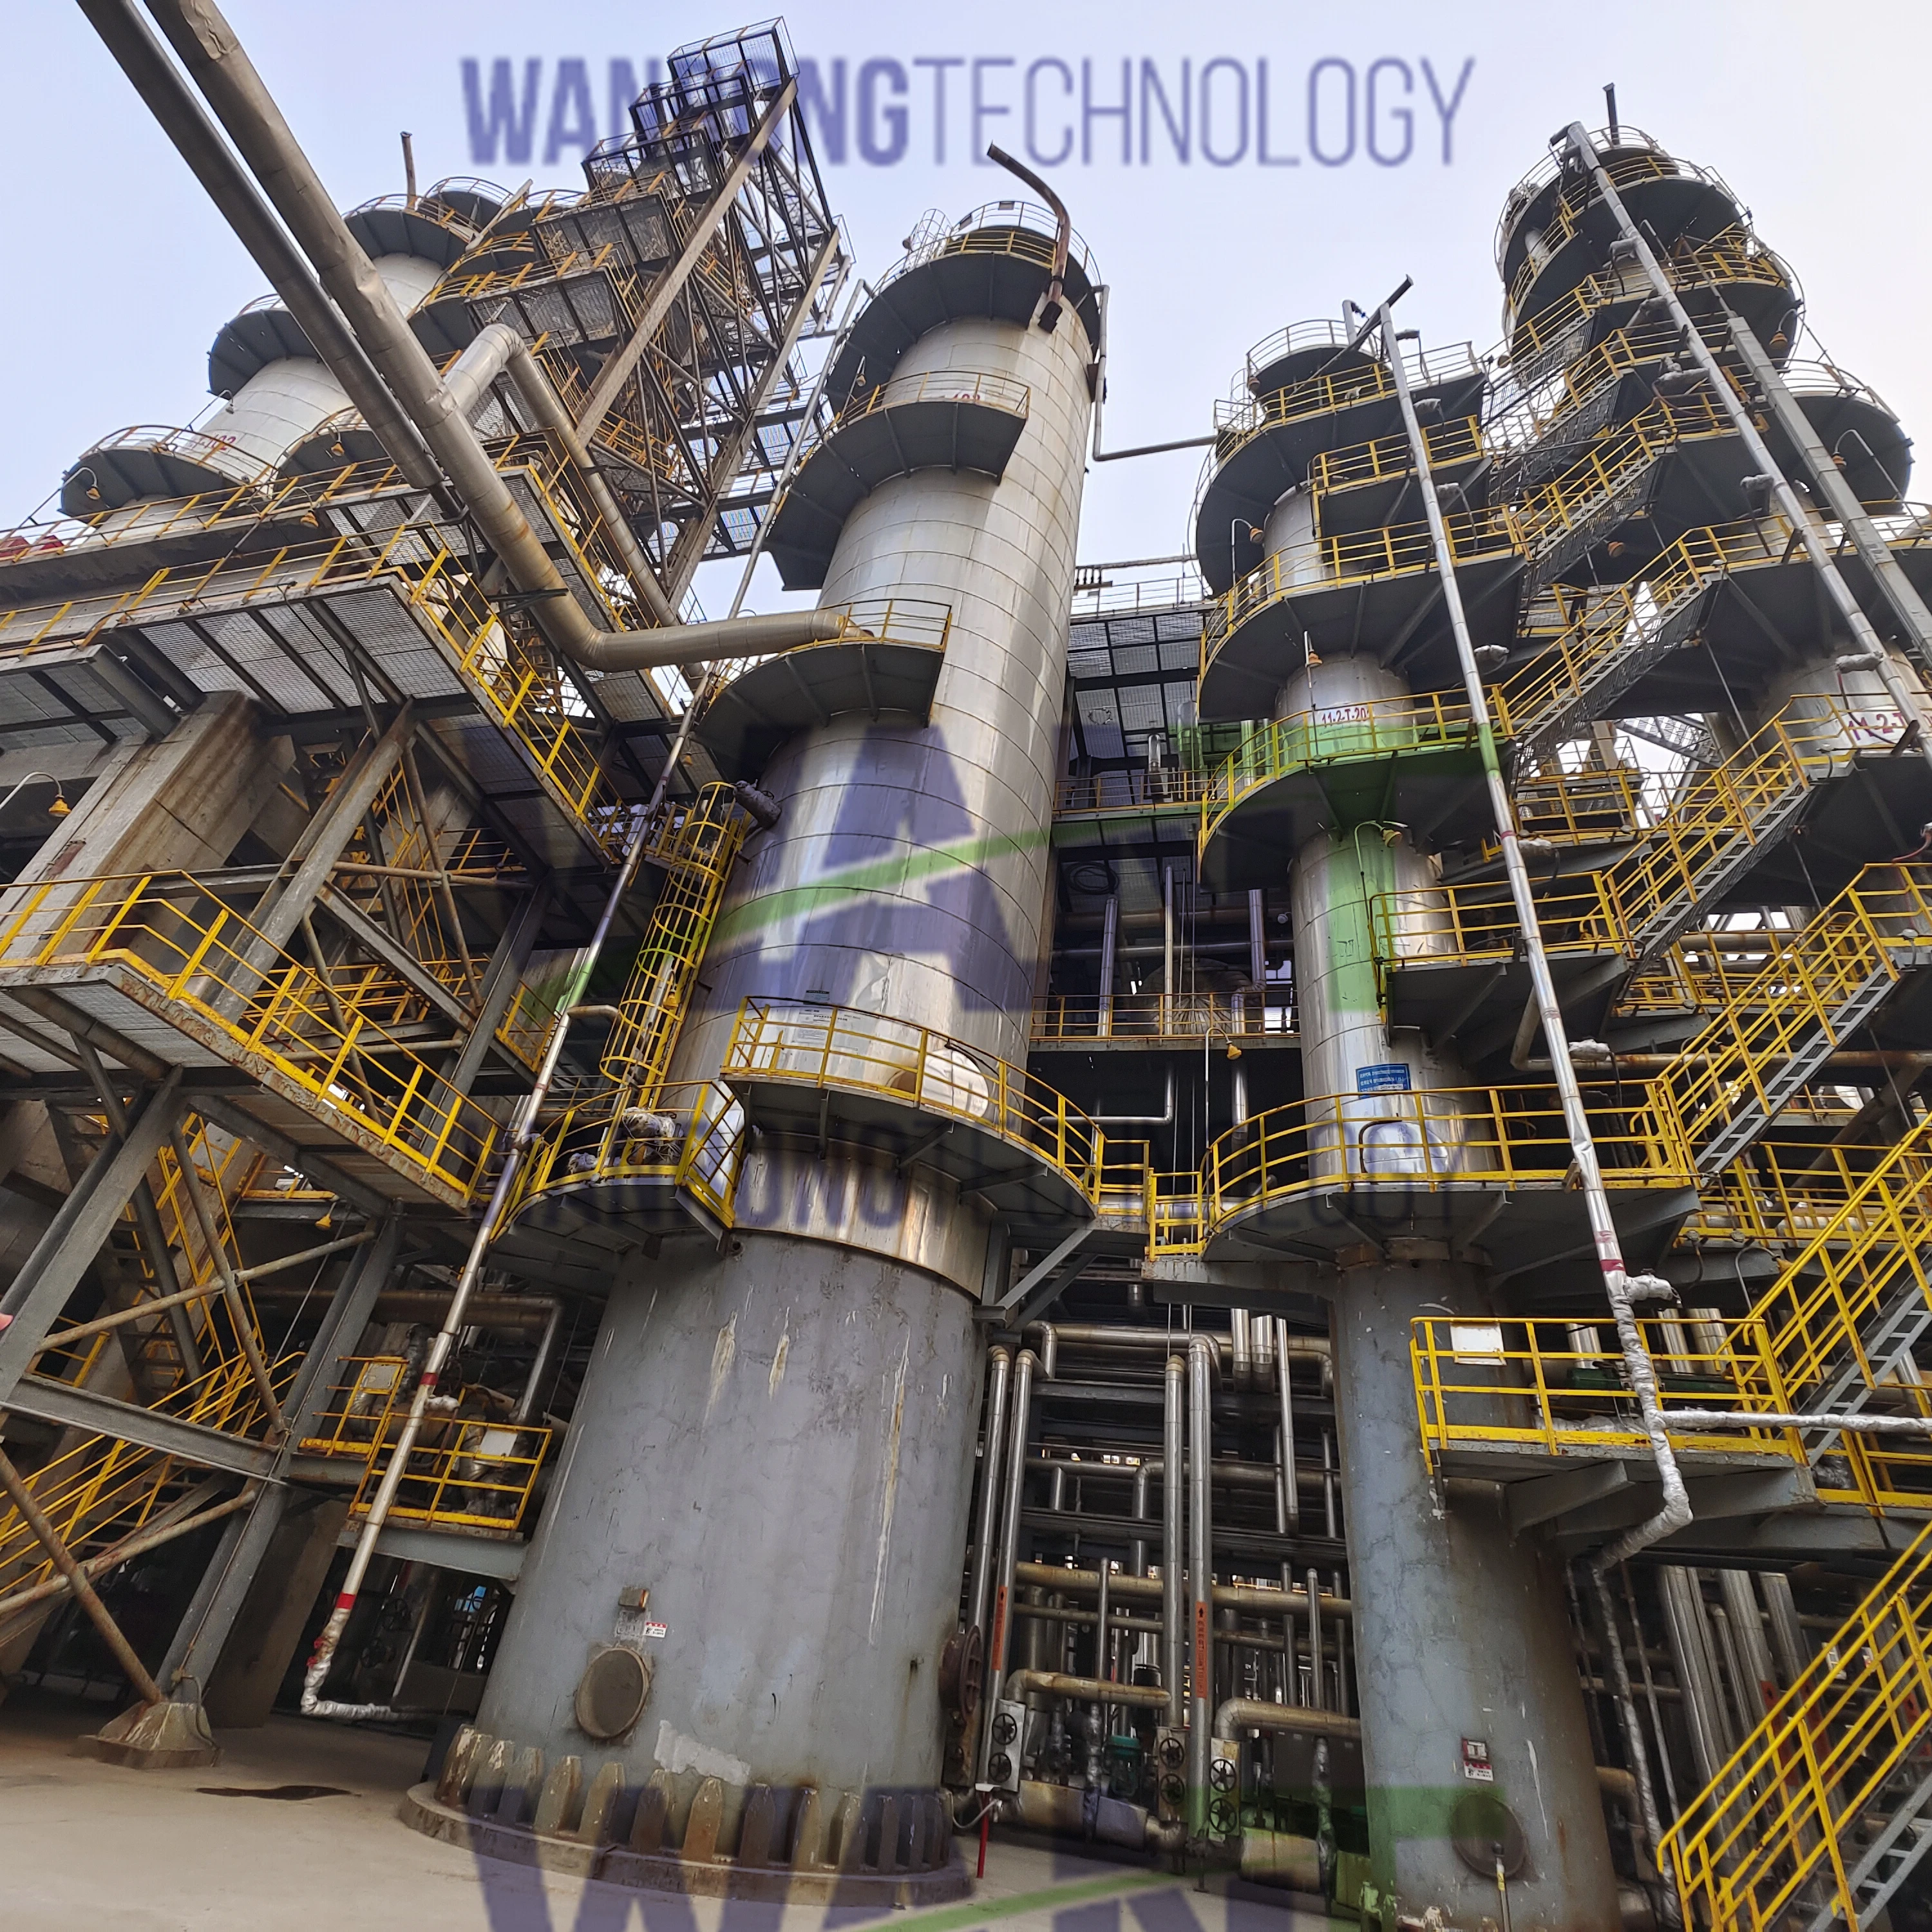
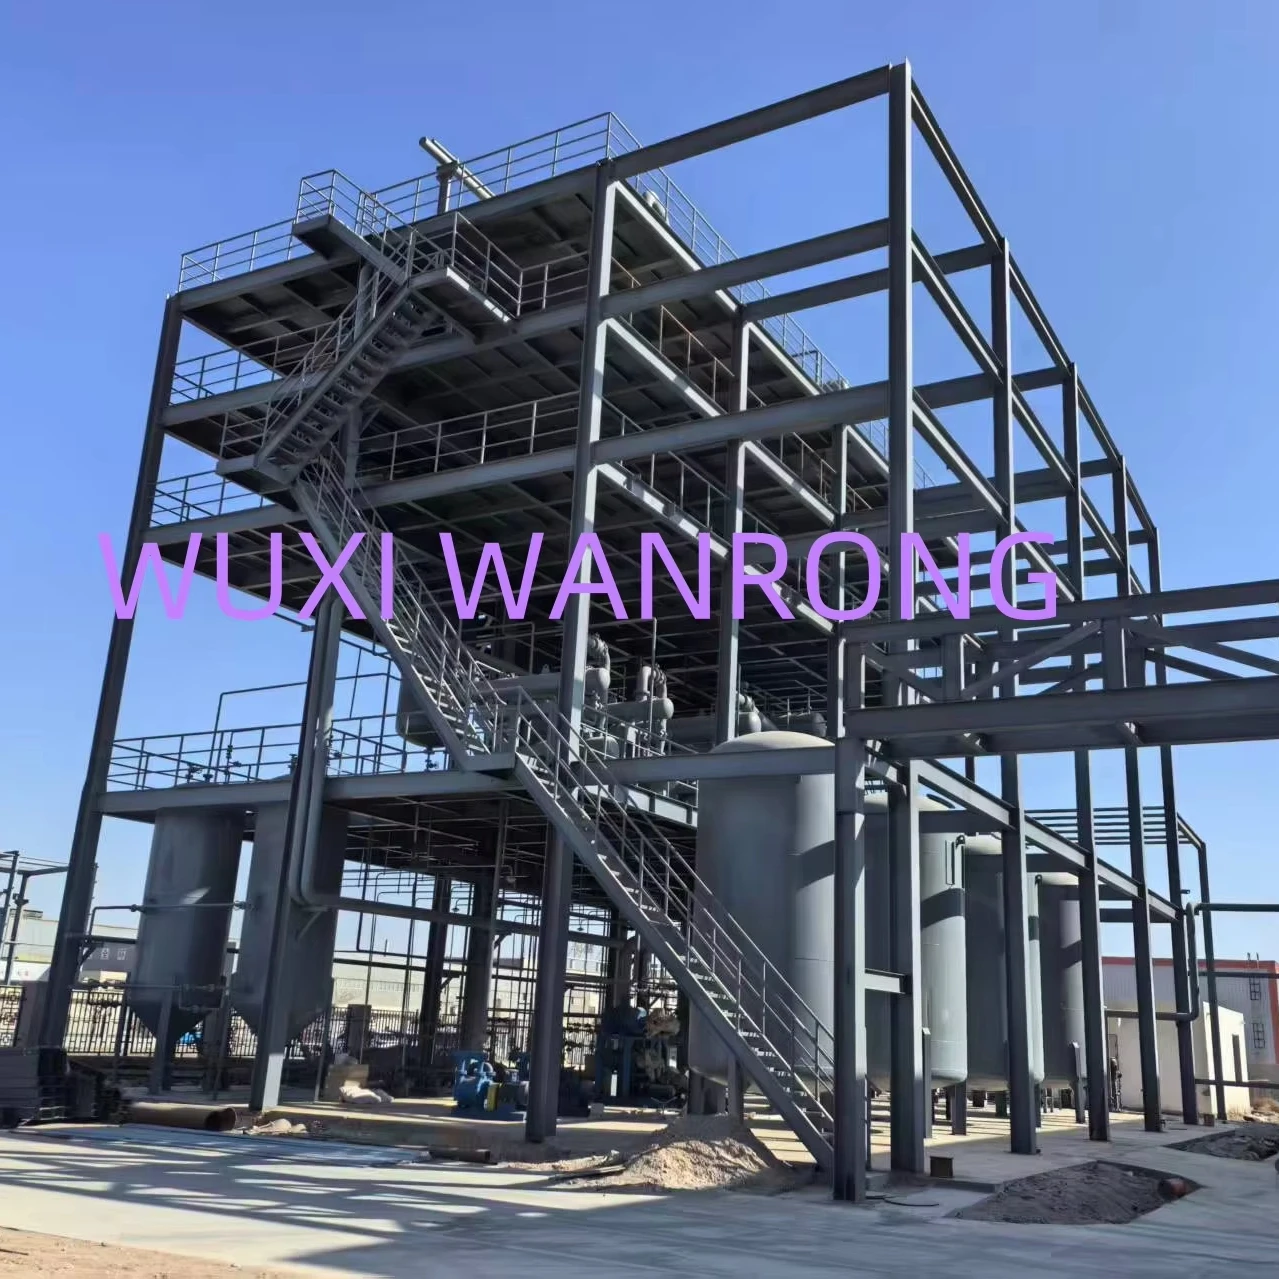
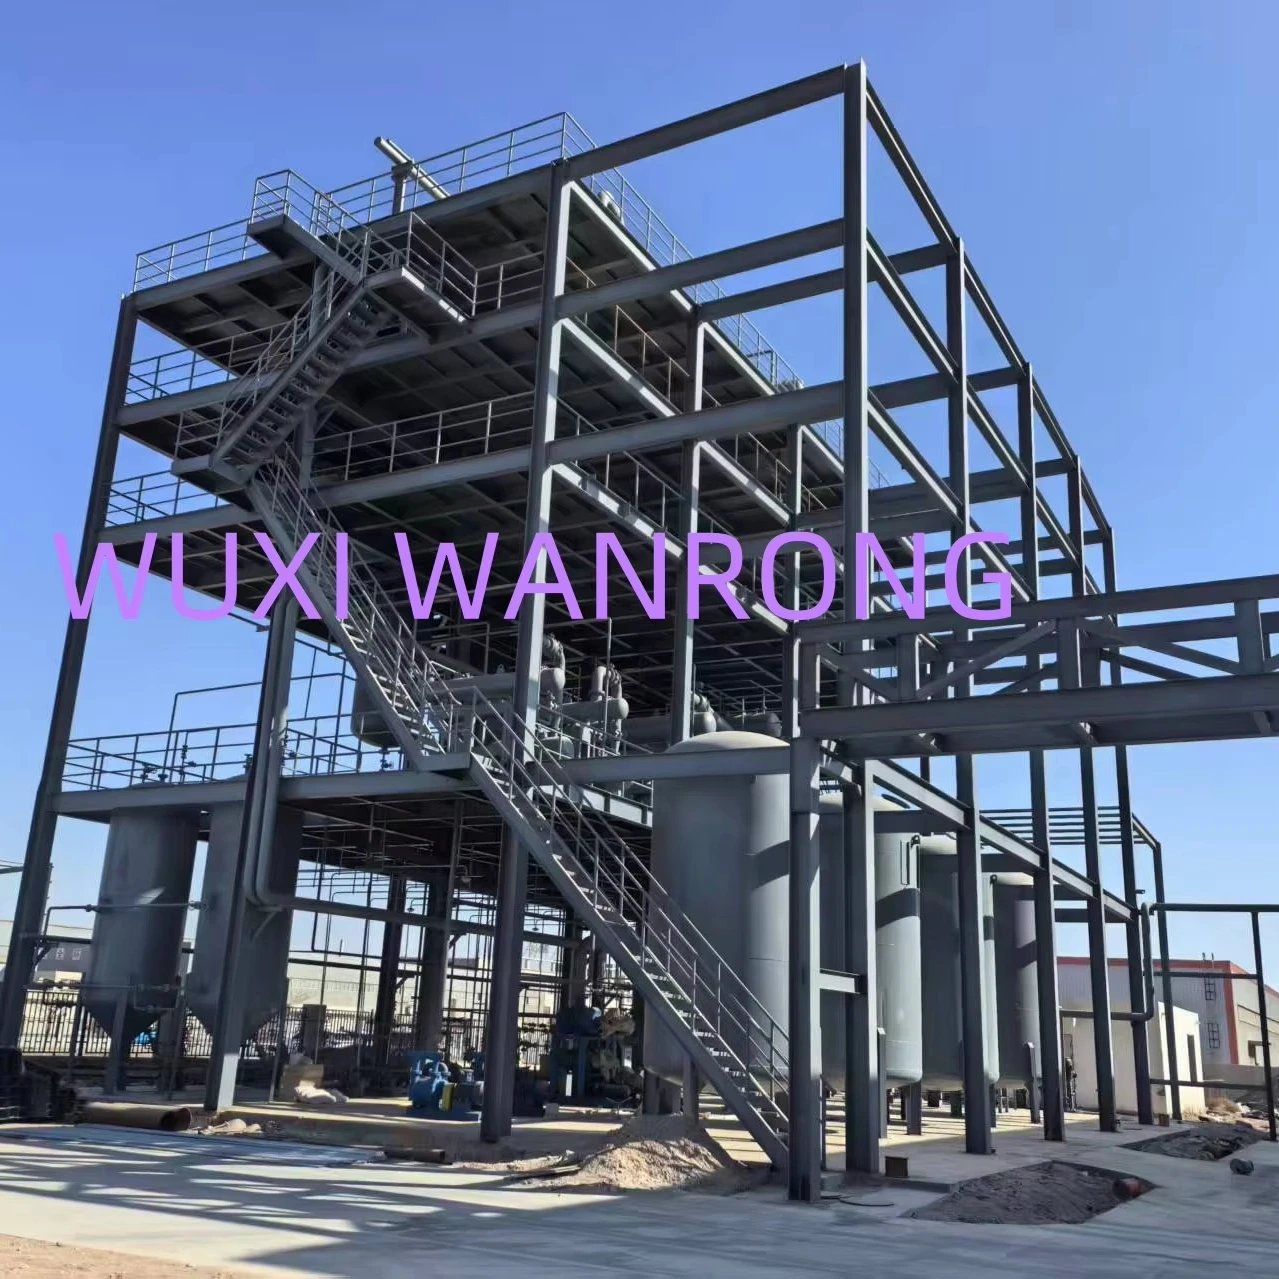
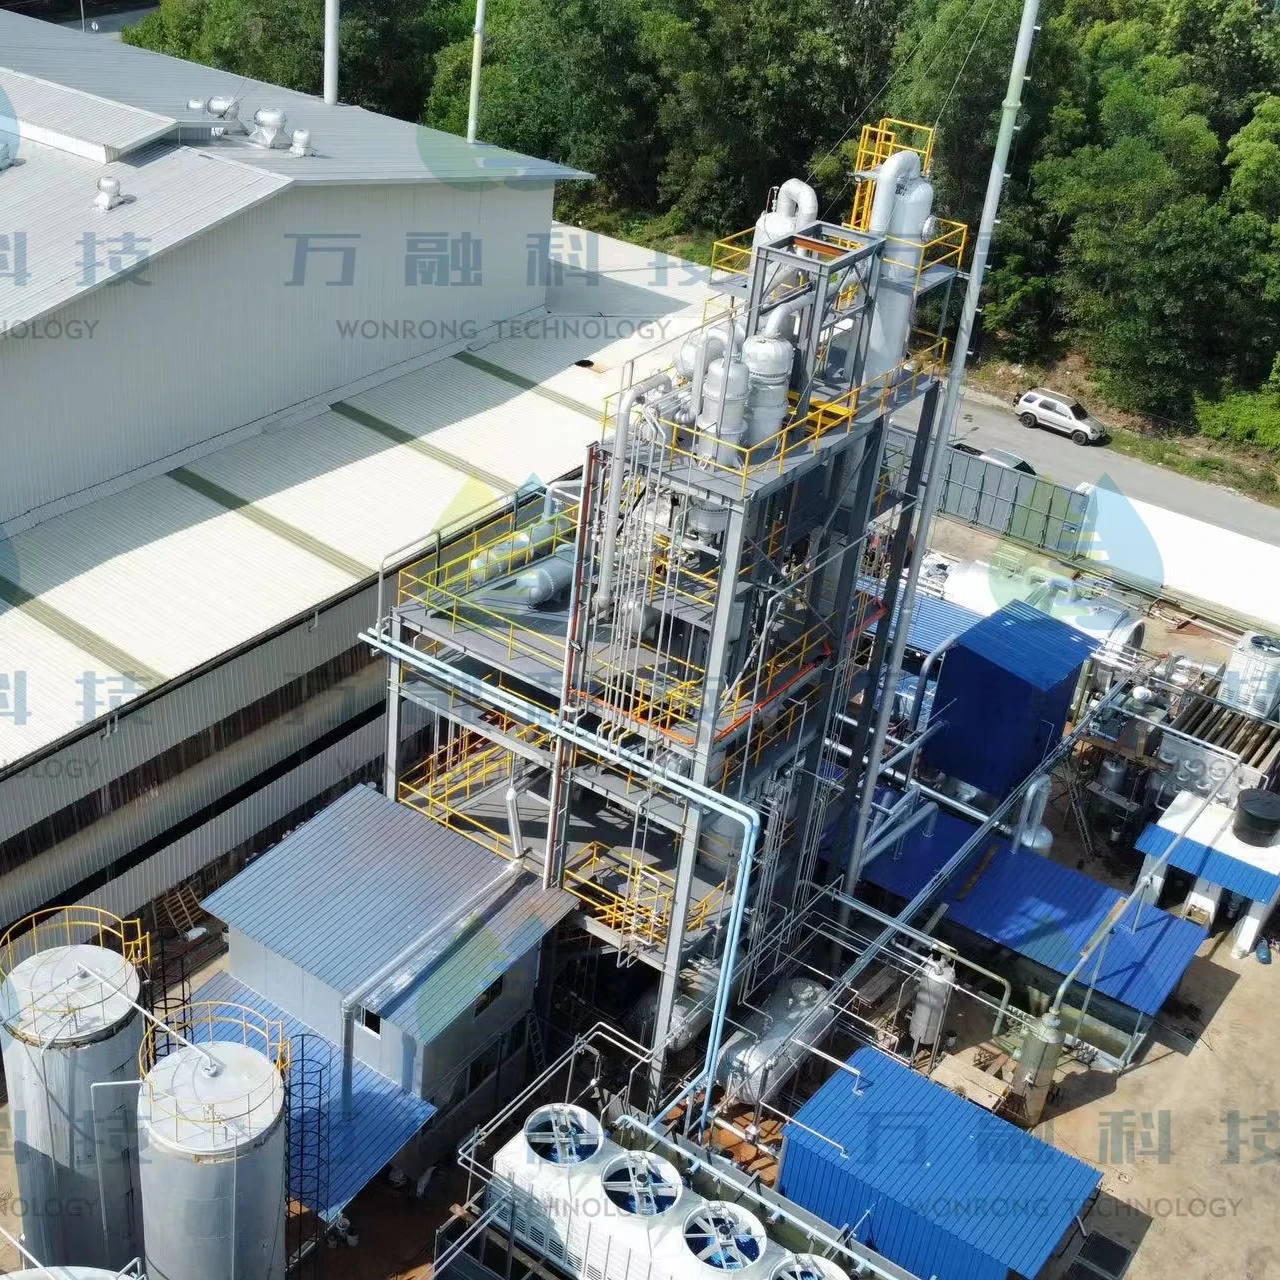
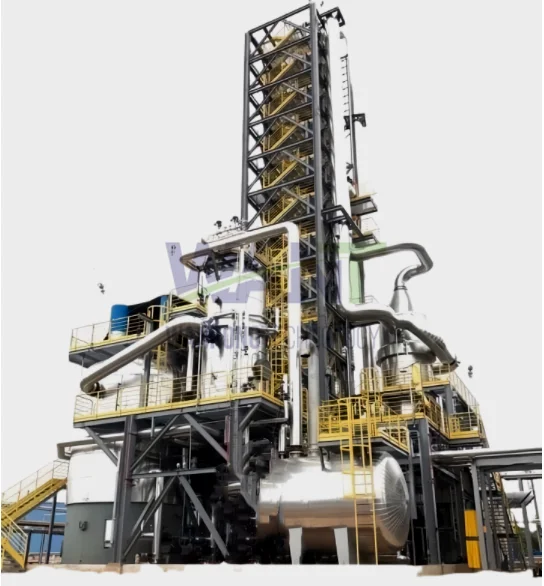
Here at WANRONG, we are delighted to provide oil industry wholesale buyers with efficient distillation towers. Our refining oil towers are used for faster, more efficient reforming of oils. With our advanced technology and professional solutions, we are dedicated to promoting the growth of production and improved quality for our customers.
Our distillation columns are built using cutting edge technology and differ from traditional stills. For years of R&D, we have never compromised on the quality and the services provided to our customers resulting in great market acceptance so far. Innovation Ranging from automatic controls and optimized heat transfer systems, our technology sets higher standards of performance and durability. Crude oil refinery
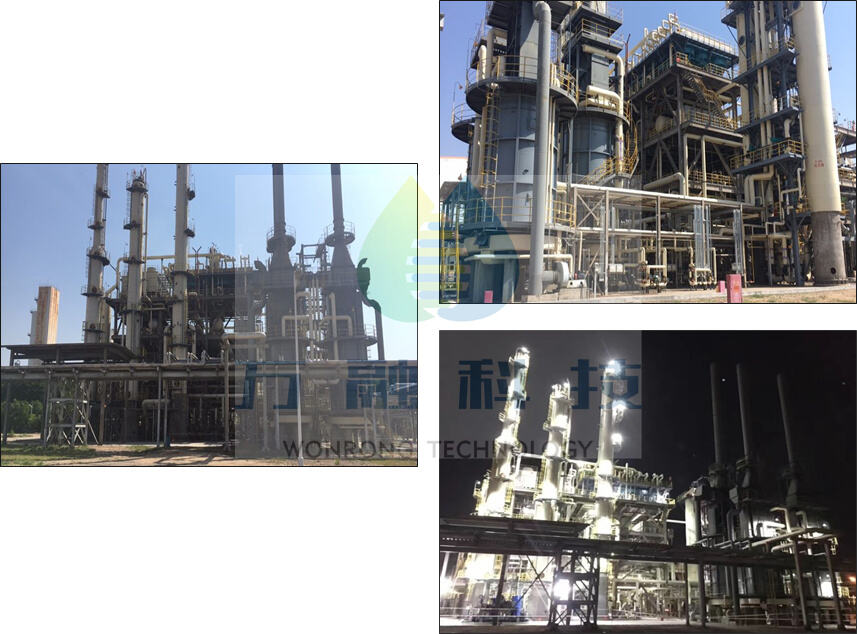
In industrial applications, product quality is key. At WANRONG,we strive to create superior oil products that adhere to industry standards. We construct our distillation towers to provide the highest quality product and enable you to get predictable results, every month. Whether you need to refine crude oil or recycle used oil, our distillation towers are ‘cutting-edge’ and will become an added value in your business. Modular refinery
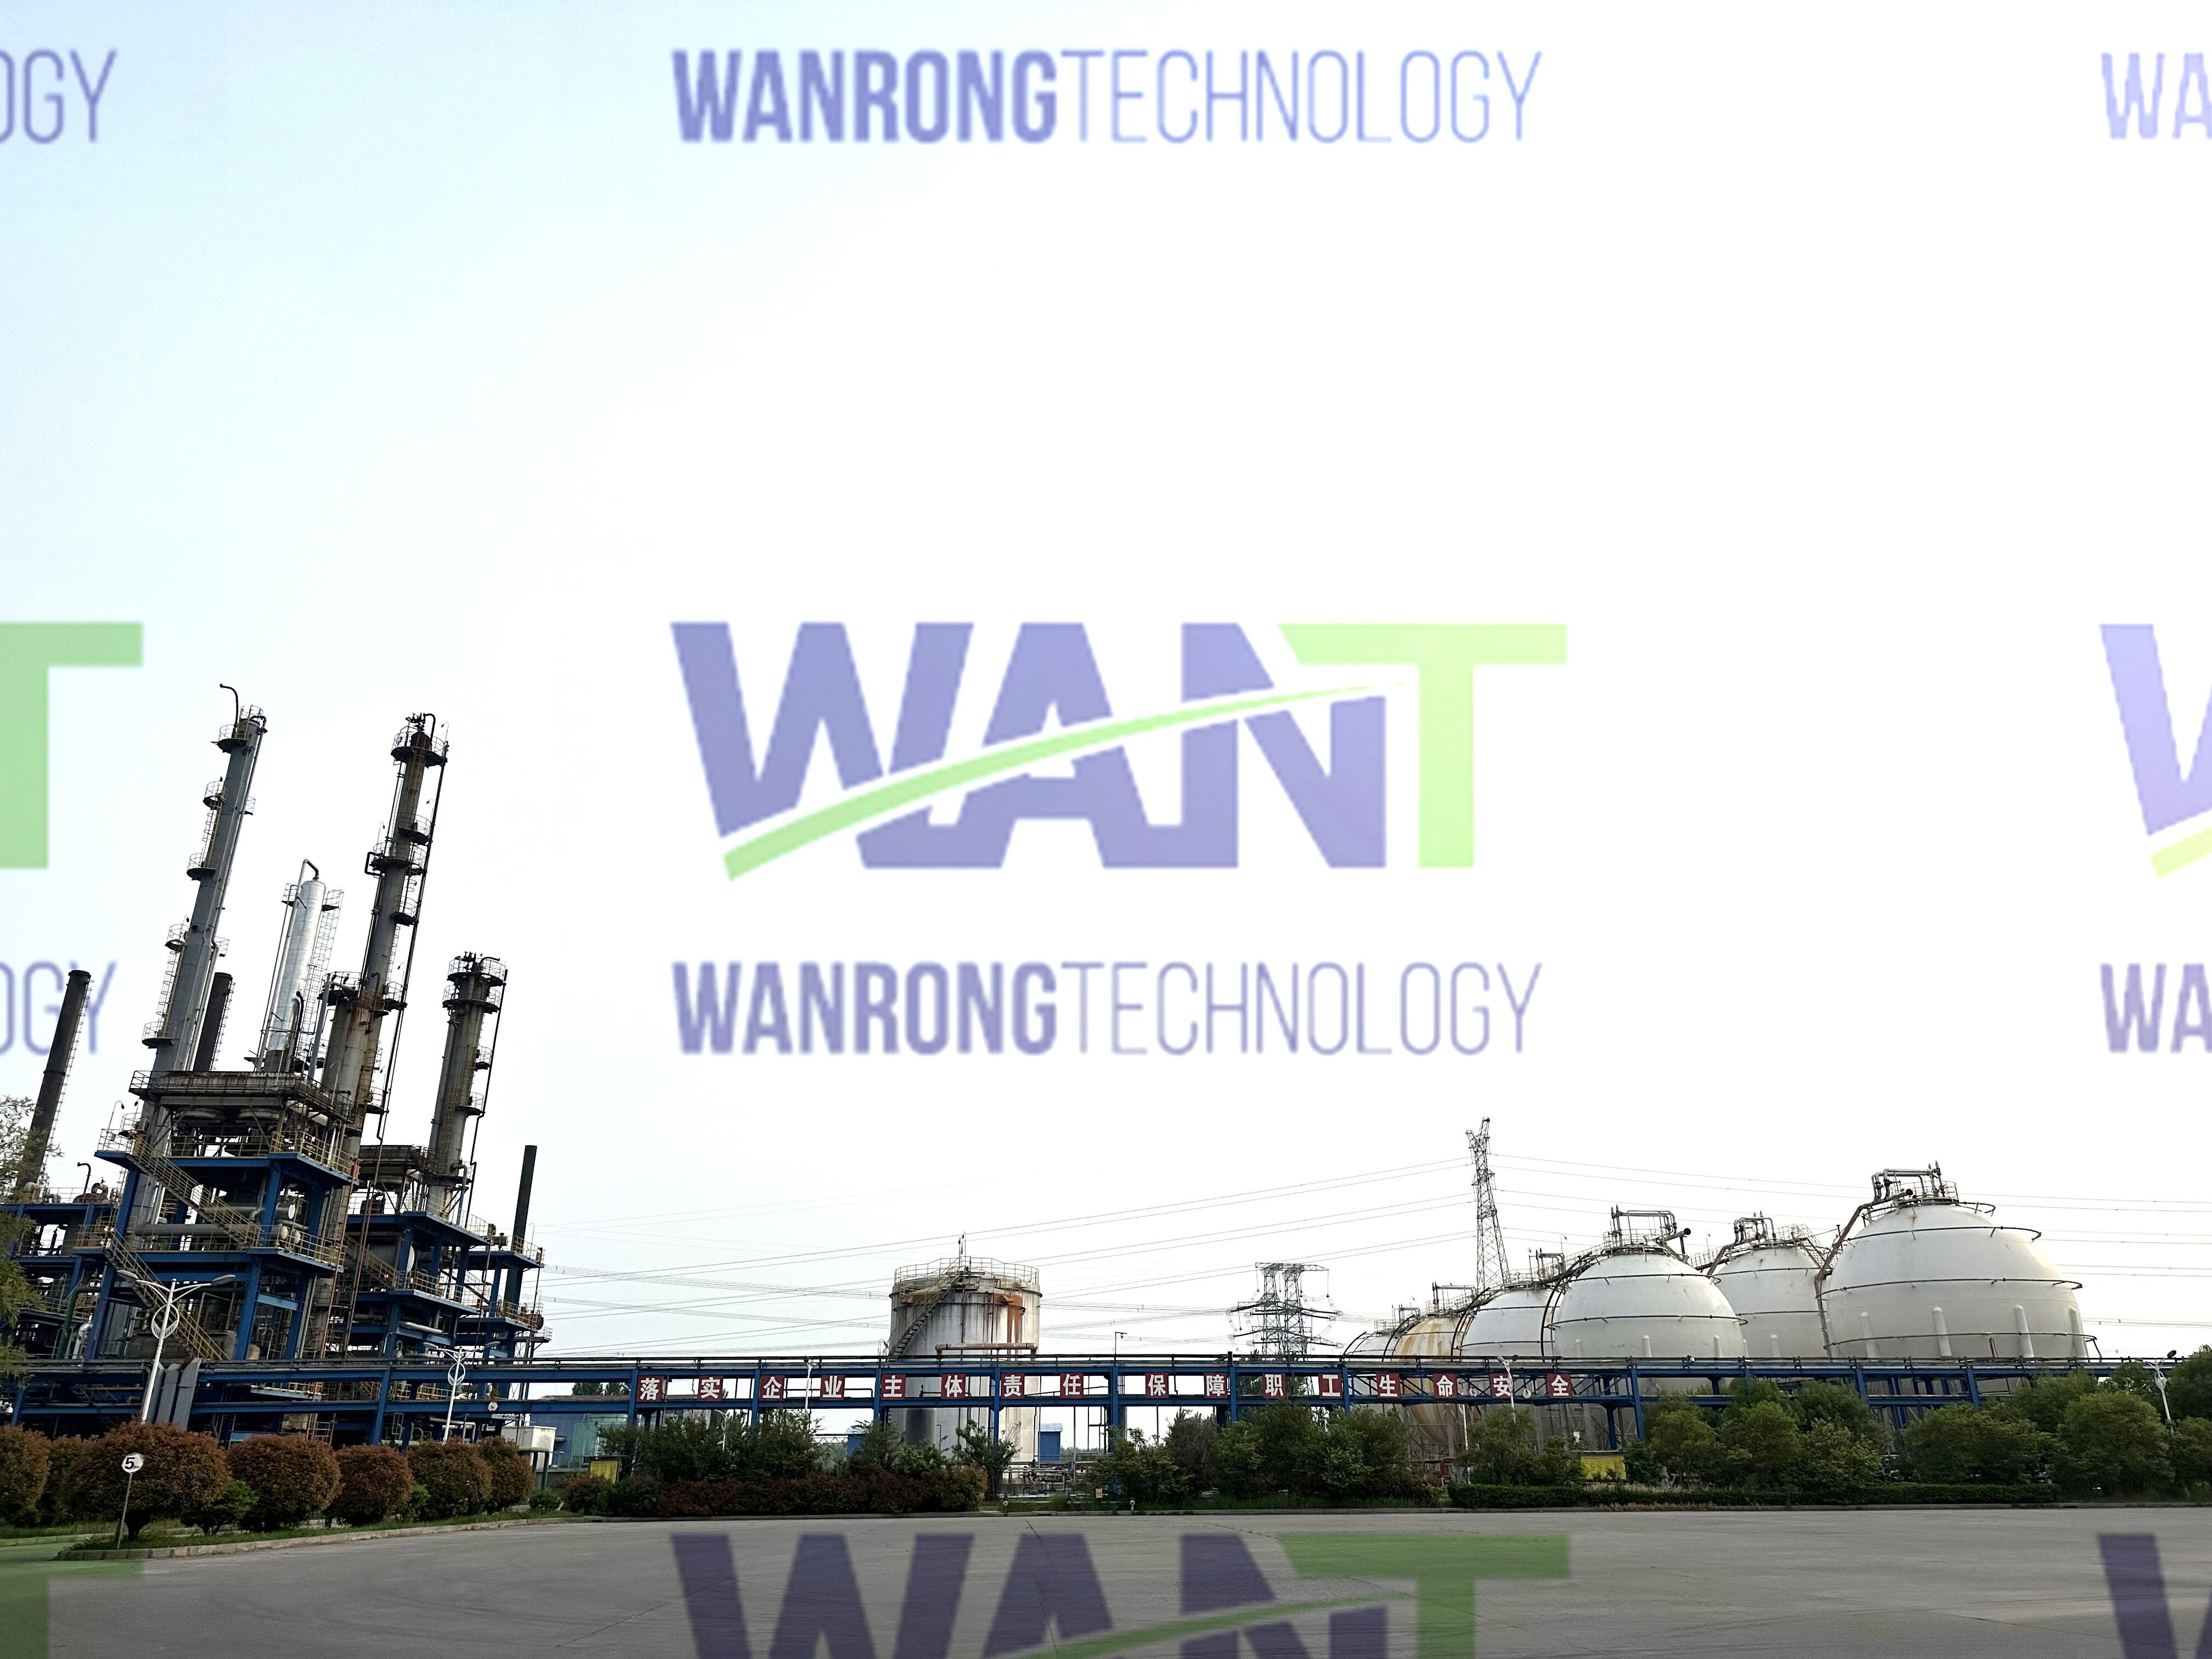
Cost is also another major factor that affects the company which is in the line of oil. which is why WANRONG has been striving to offer cost-effective handling solutions when it comes to oil refinery. Our distillation column are engineered for low energy consumption and to reduce overall operating costs, allowing our customer to realize large savings over its life. Through our affordable options companies can improve the financial aspect of their business without sacrificing quality. Waste oil recycling
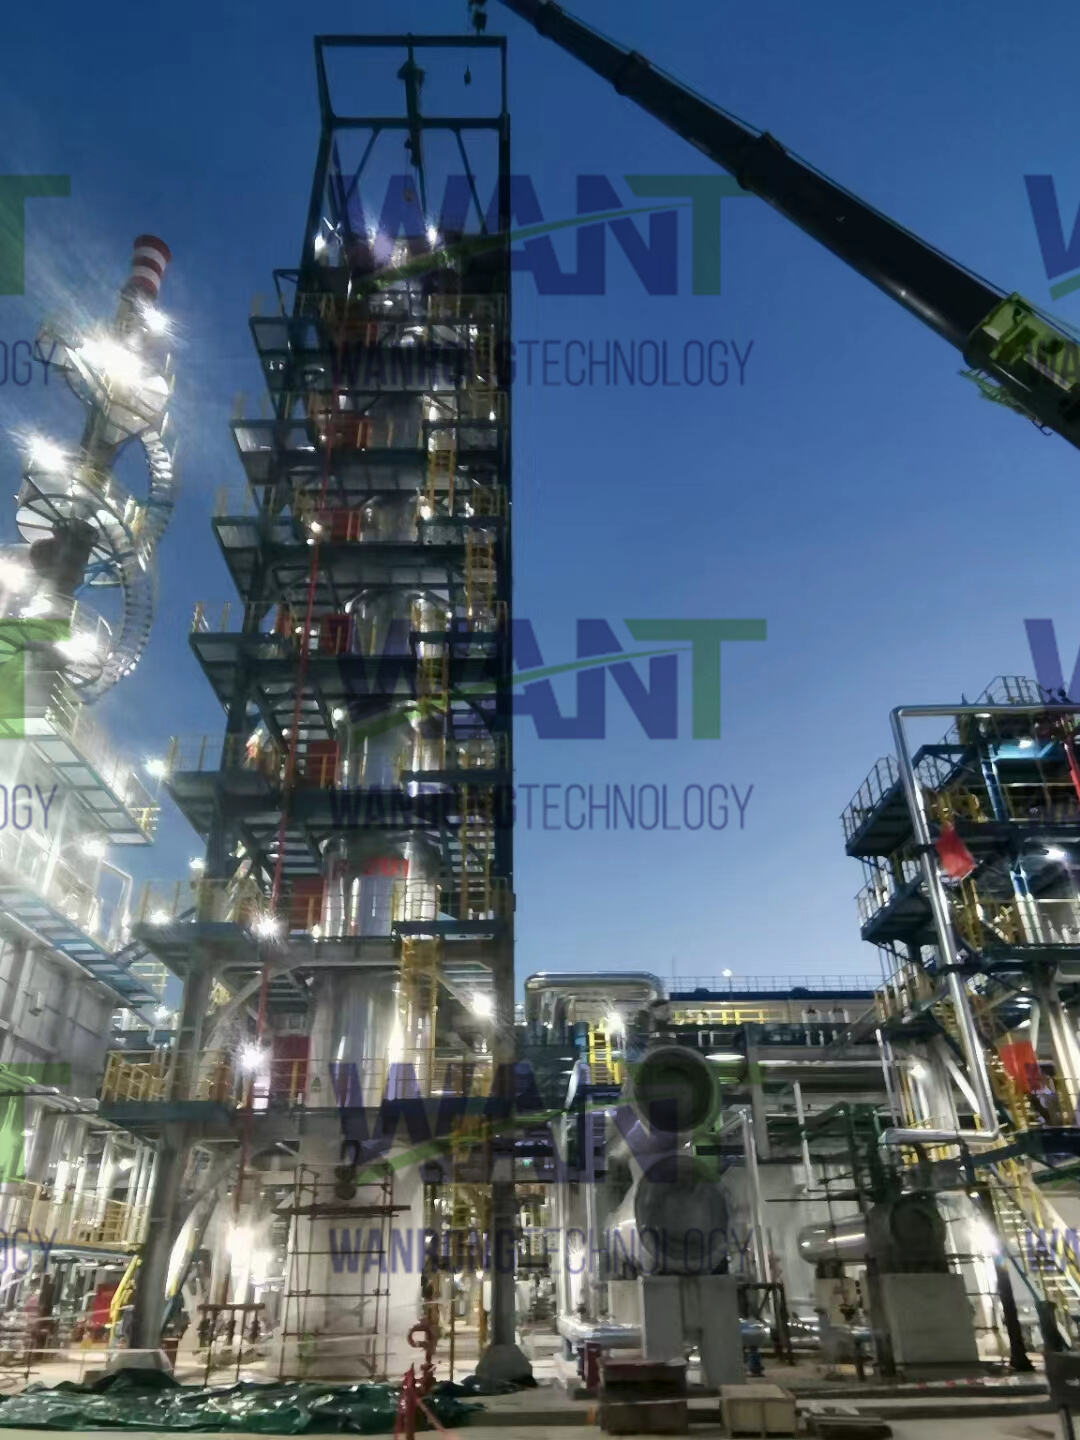
This is especially true in the type of oil distillation. Our distillation columns are designed for consistent performance to deliver maximum yield and minimal downtime. With heavy-duty construction and innovative features, our towers proudly stand alone in some of the toughest industrial applications. At WANRONG, we work to ensure our solutions are designed with patients in mind to make them easy to use and offering enhanced functionality.
We offer advanced, integrated technologies across the hydrocarbon value chain—from waste oil regeneration, crude oil hydrogenation, and high-purity gas separation to API-certified base oil production—enabling clients to achieve both profitability and environmental compliance.
Our close cooperation with top research institutes like Sinopec Shanghai and Nanjing Chemical Research Institute ensures continuous technological advancement, validated through rigorous simulation using Aspen and Plant 3D, keeping us at the forefront of hydrocarbon processing and environmental solutions.
We provide customized, turnkey EPC/EPCC solutions—from design and simulation to fabrication, testing, and commissioning—supported by a worldwide service network to ensure efficient, reliable project execution for clients across Asia, Africa, the Middle East, and beyond.
Adhering to stringent international standards (ASME, PED, ISO, API) and implementing a full-cycle QC system with 217+ checkpoints, we ensure every piece of equipment meets exacting specifications for performance, safety, and durability in global markets.
Copyright © Wuxi Wanrong Environmental Protection Technology Co.,Ltd. All Rights Reserved

 EN